
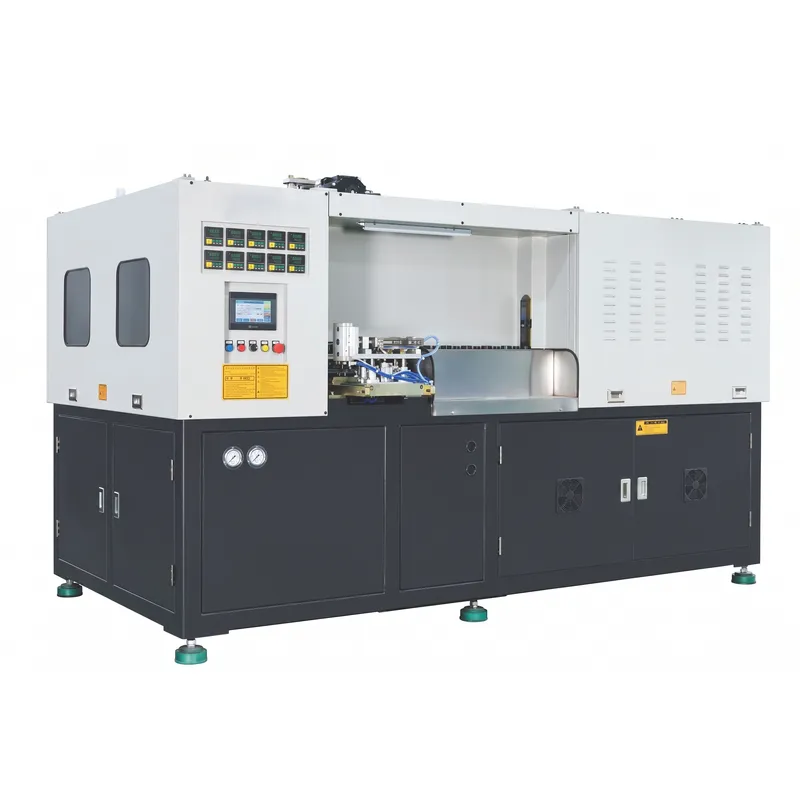
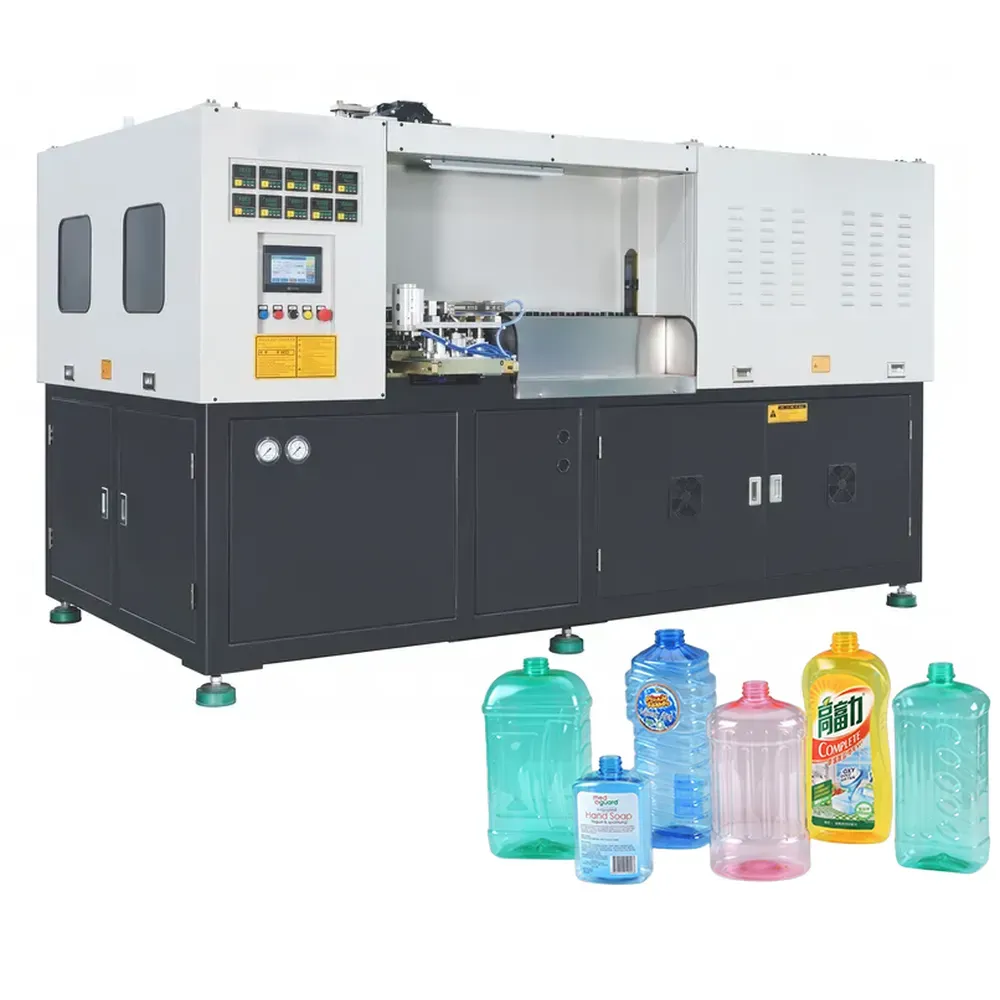
EPA.ES-3C114 Máquina de moldeo por soplado totalmente automática para botellas de productos químicos de uso diario y cosméticos.
La EPA.ES-3C114 es una máquina de moldeo por soplado automática de alto rendimiento, diseñada específicamente para la producción diaria de botellas para productos químicos y cosméticos. Equipada con servomotores de renombre internacional, reductores de precisión y sistemas de control eléctrico avanzados, esta máquina automática de moldeo por soplado de PET ofrece el funcionamiento estable, fiable y energéticamente eficiente que exigen las líneas de envasado modernas. Como máquina de moldeo por soplado de botellas cosméticas diseñada específicamente para este fin, la EPA.ES-3C114 destaca con materiales PET y PETG, produciendo una amplia gama de formas y acabados de cuello en tres cavidades simultáneamente.
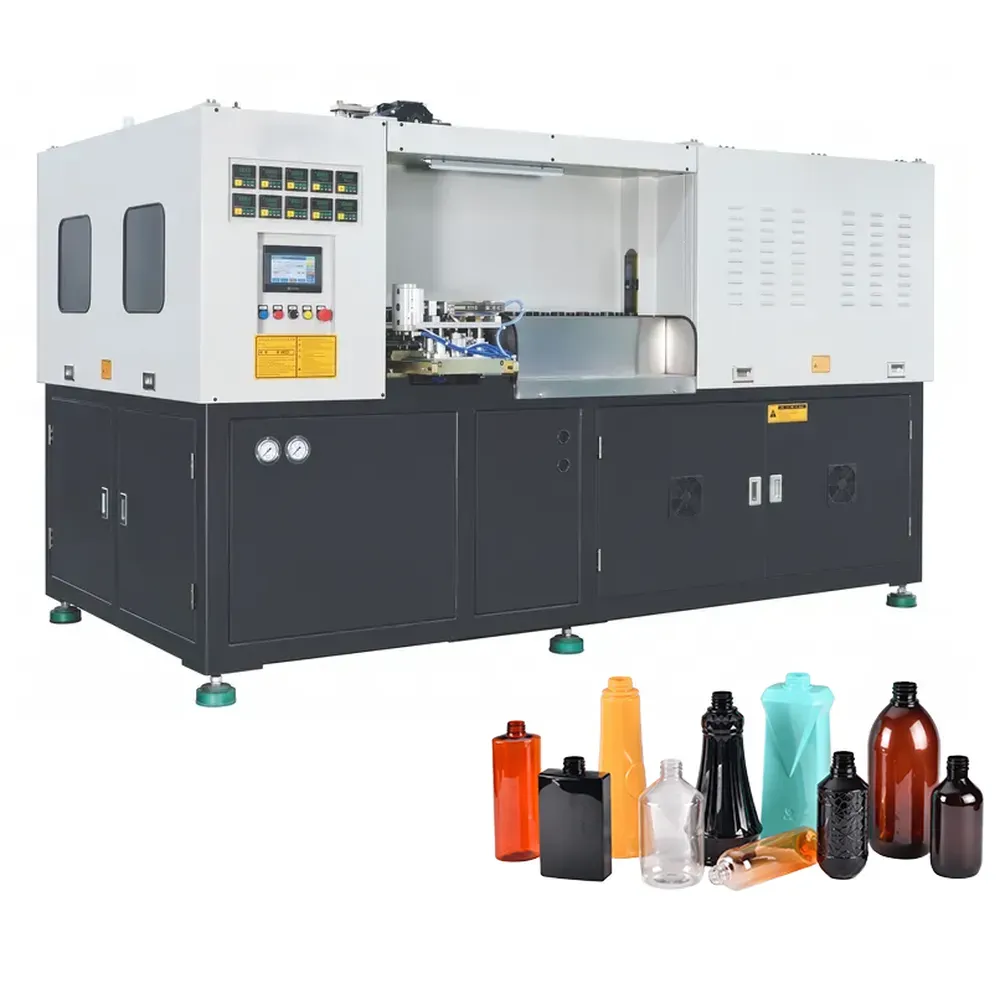
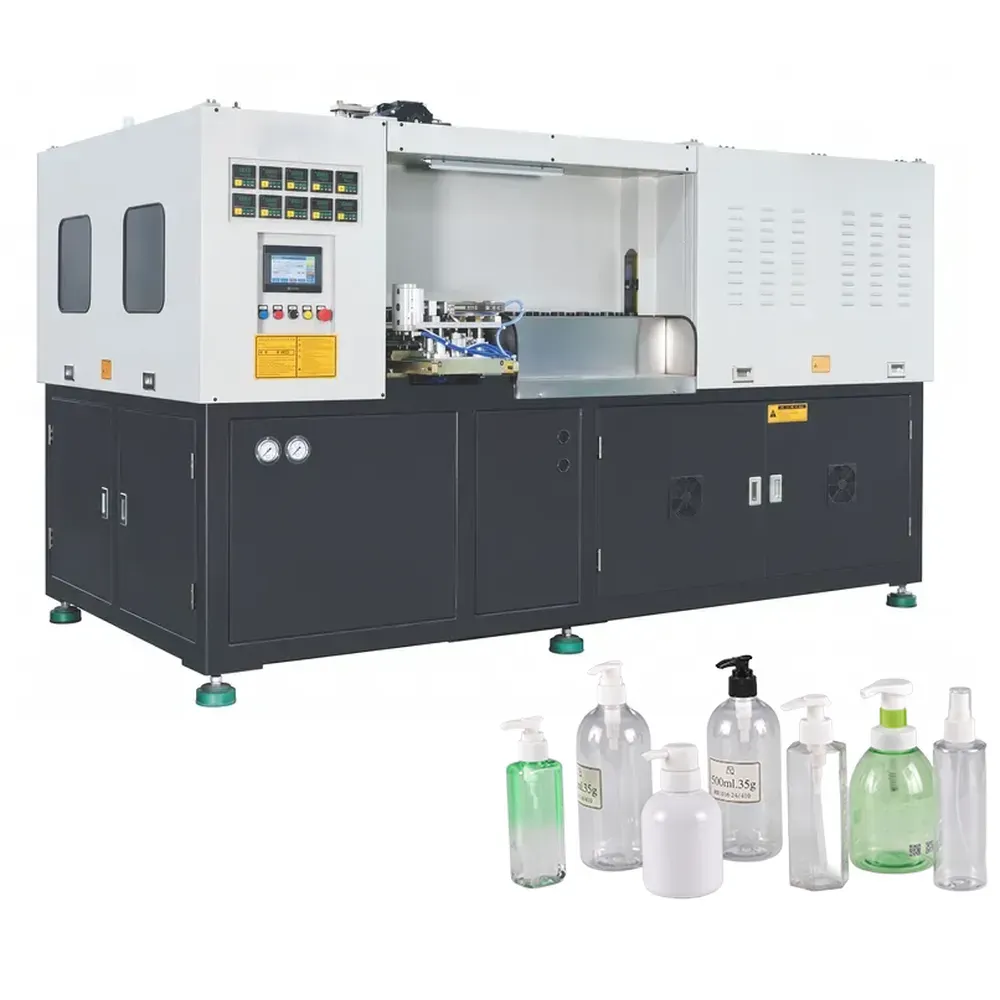
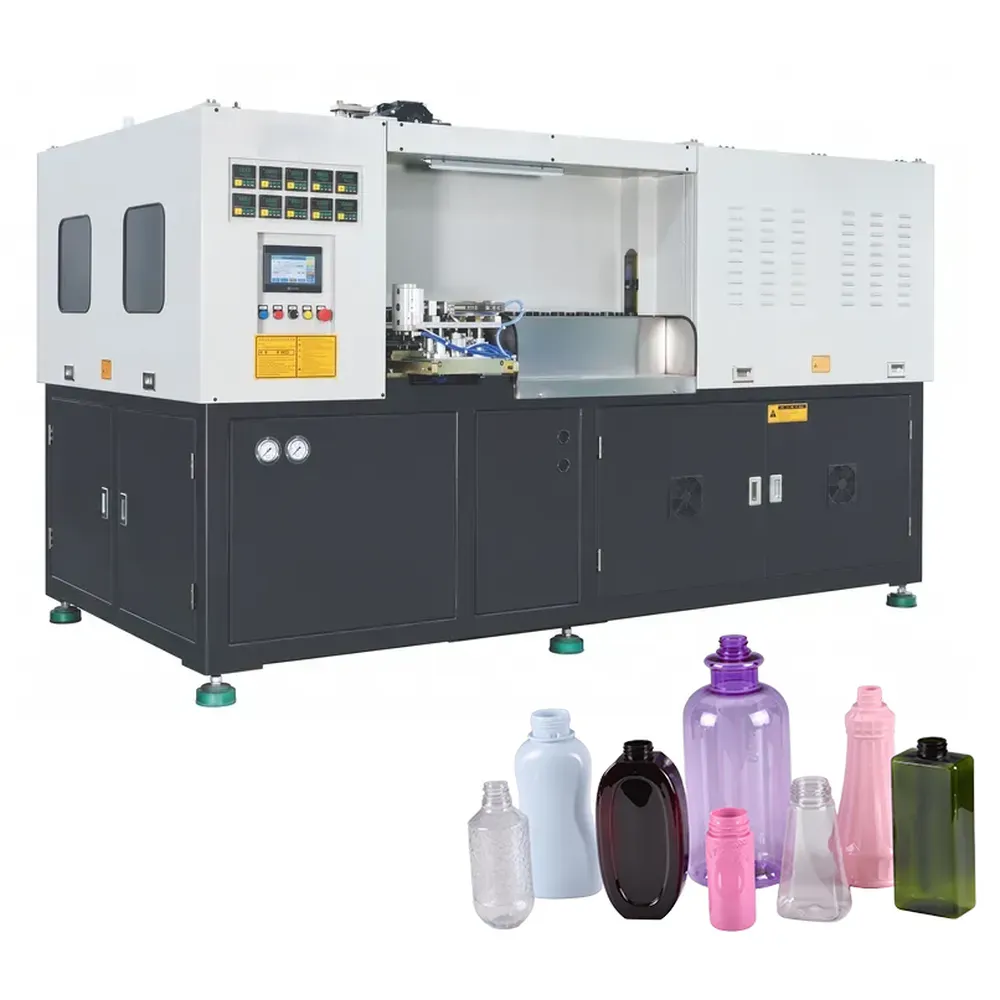
The EPA.ES-3C114 is a high-performance fully automatic blow molding machine engineered specifically for daily chemical and cosmetic bottle production. Built around internationally renowned servo motors, precision reducers, and advanced electrical control systems, this automatic PET blow molding machine delivers the stable, reliable, and energy-efficient operation that modern packaging lines demand. As a purpose-built cosmetic bottle blow molding machine, the EPA.ES-3C114 excels with PET and PETG materials, producing a wide range of bottle shapes and neck finishes across 3 cavities simultaneously. Its particular strength lies in manufacturing complex, irregularly shaped bottles that challenge standard equipment, making it a preferred plastic blow molding machine for premium cosmetic and personal care brands. With a theoretical output of 2,400 bottles per hour and a compact footprint of 3,240 x 1,800 x 2,000mm, it suits both greenfield installations and factory-floor upgrades where space efficiency matters.
As a versatile daily chemical bottle blow molding machine, the EPA.ES-3C114 handles container volumes from 30ml to 1,500ml, covering toner bottles, lotion containers, serum dispensers, shampoo bottles, and body wash packaging in a single machine platform. The servo-driven injection stretch blow molding machine architecture guarantees repeatable wall thickness, accurate neck finishes, and high transparency in the finished container. Its user-friendly interface reduces operator learning time, while optimized energy management makes this industrial blow molding machine an economical long-term investment. By combining high molding precision with broad material applicability, the EPA.ES-3C114 helps manufacturers scale output, control production costs, and raise product quality to meet the increasingly demanding standards of global cosmetic and daily chemical markets. For buyers evaluating types of blow molding machine technology for cosmetic packaging, this model represents the current benchmark in its class.
Parámetro técnico
| Modelo | Unidad | EPA.ES-3C114 | |
|---|---|---|---|
| Moldura | Carrera de sujeción | mm | 133 |
| Distancia de apertura del molde | mm | 363 | |
| Distancia de moldeo | mm | 230 | |
| Trazo de estiramiento | mm | 350/450 | |
| Distancia de apertura del molde | mm | 50 | |
| Distancia de moldeo | mm | 114 | |
| Soporte para preformas | 74 | ||
| Caries | 3 | ||
| Recipiente | Volumen máximo del contenedor | ml | 1500 |
| Rango de diámetro del cuello | mm | 40 | |
| Diámetro máximo del contenedor | mm | 95 | |
| Altura máxima del contenedor | mm | 250/330 | |
| Salida teórica | hiperplasia prostática benigna | 2400 | |
| Sistema eléctrico | Potencia máxima de calentamiento | kw | 40 |
| Potencia de calefacción | kw | 18 | |
| Sistema de aire | Presión de funcionamiento | kg/cm² | 7 |
| Consumo de aire a baja presión | litros/min | 1500 | |
| Presión de soplado | kg/cm² | 35 | |
| Consumo de aire a alta presión | litros/min | 3200 | |
| agua de refrigeración | Presión de funcionamiento | kg/cm² | 5-6 |
| Temperatura | °C | 8-12 | |
| Caudal | litros/min | 30 | |
| Máquina | Tamaño (L*An*Al) | mm | 3240*1800*2000 |
| Peso | kg | 4000 | |
Features of the EPA.ES-3C114 Cosmetic Bottle Blow Molding Machine
1. High-Quality and Reliable Core Components
Every critical component in the EPA.ES-3C114 is sourced from internationally renowned suppliers, including servo motors, precision reducers, and electrical and control elements. This ensures stable and durable operation from the very first production cycle. The servo control system responds with exceptional sensitivity and high control accuracy, which directly reduces the machine failure rate and extends equipment service life well beyond industry averages. Manufacturers investing in a quality blow molding machine will find this component strategy delivers lower total cost of ownership across multi-year production runs.
2. Strong Adaptability and Diverse Bottle Styles
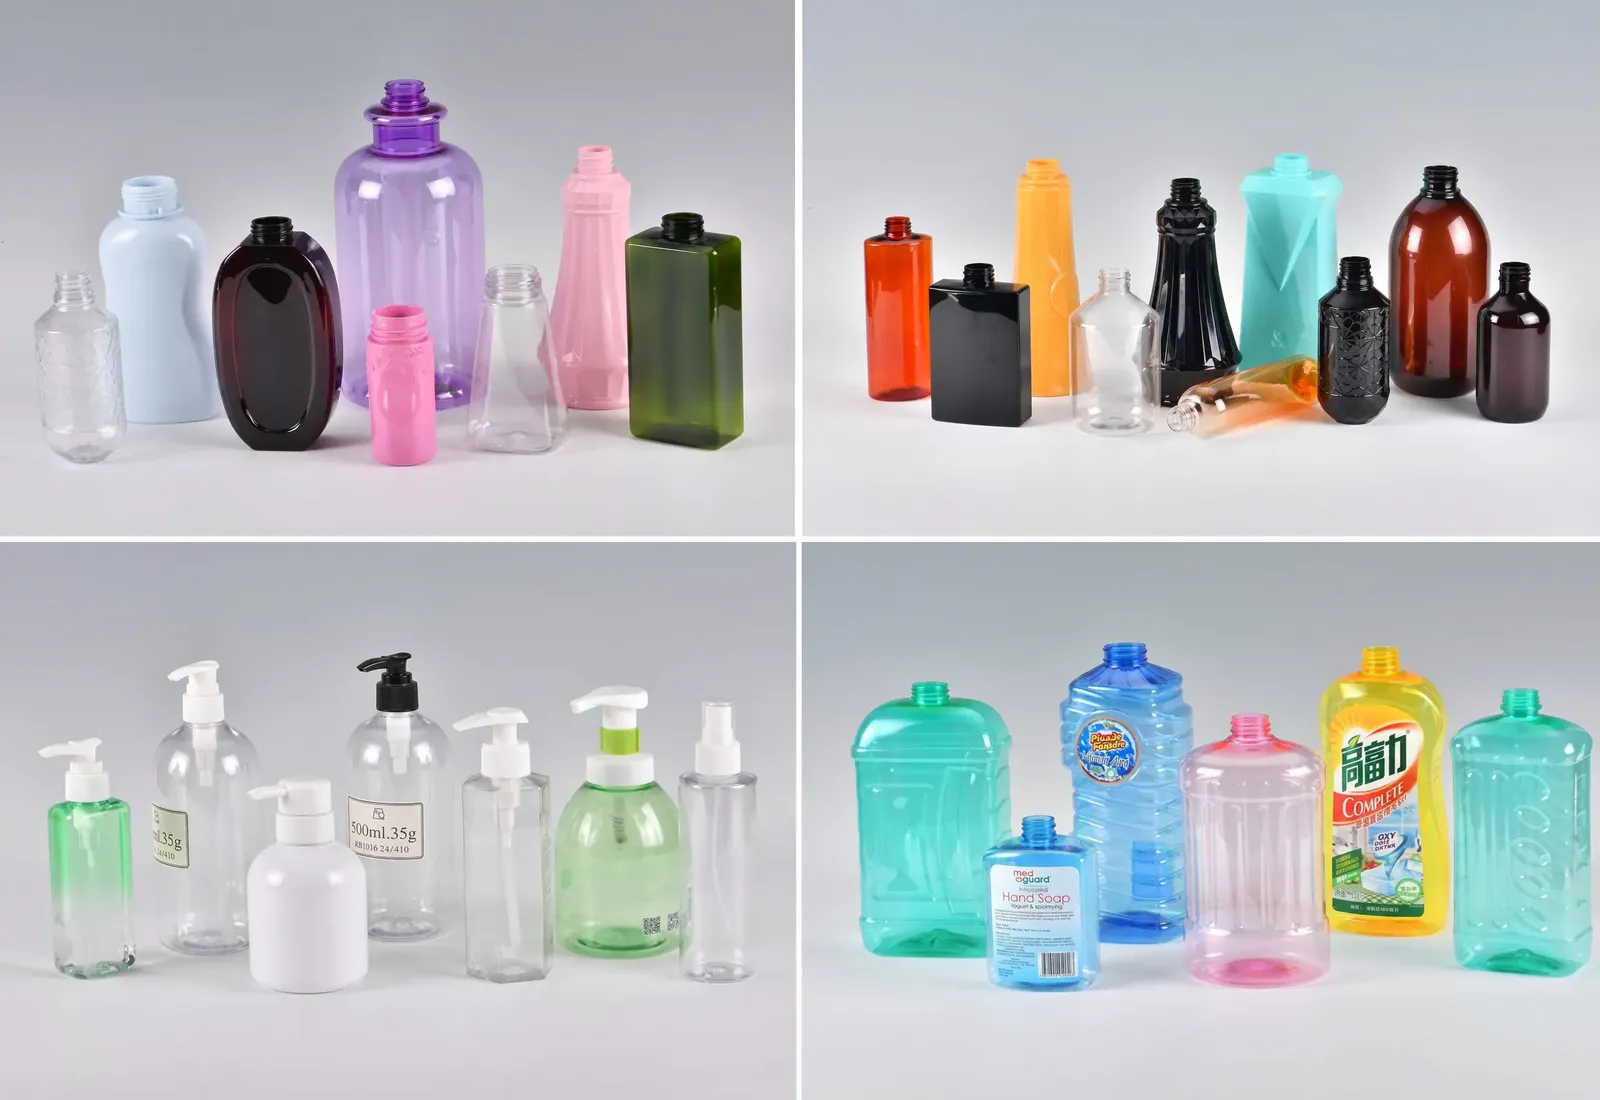
The ES-3C114 series covers a broad range of model configurations, capable of producing bottles from 30ml to 1,500ml. Body diameter, container height, and neck dimensions are all flexibly adjustable. Processing PET and PETG materials with equal precision, this PET bottle blow molding machine handles standard cylindrical bottles and highly complex irregular shapes with consistent quality. It serves as a professional plastic bottle blow molding machine for lotion, toner, serum, shampoo, conditioner, hand sanitizer, and specialty cosmetic packaging, providing a single versatile platform for diverse SKU portfolios across cosmetic and daily chemical product lines.
3. High Efficiency and Energy Savings
The electrical system operates with a max heating power of 40kW and a working heating power of 18kW, combining servo drive technology to significantly reduce energy consumption compared to conventional hydraulic systems. The blowing system achieves a maximum pressure of 35 kg/cm², delivering high blow molding efficiency with a theoretical output of 2,400 bottles per hour across 3 cavities. This makes the EPA.ES-3C114 a genuine high speed blow molding machine for cosmetic and daily chemical production. Manufacturers switching from older equipment will experience measurable reductions in electricity costs alongside increased throughput, which directly improves per-unit production economics at scale.
4. High Stability and Easy Maintenance
The EPA.ES-3C114 features a scientifically optimized structural design with a cooling water system maintaining temperatures between 8 and 12 degrees Celsius, ensuring consistent bottle molding quality across long production runs. Air pressure parameters and electrical systems are pre-configured to optimal ranges, resulting in a low failure rate under continuous operation. Daily maintenance routines are straightforward, with accessible service points reducing downtime and labor costs. For production managers running multiple shifts, the machine's operational stability translates directly into predictable output schedules and reduced unplanned maintenance events throughout the equipment's service life.
5. Compact Structure and Small Footprint
At 3,240 x 1,800 x 2,000mm and 4,000kg, the EPA.ES-3C114 is engineered with a compact, factory-floor-friendly footprint that makes layout planning straightforward even in constrained workshop spaces. This size profile is particularly valuable for cosmetic manufacturers operating in urban manufacturing parks or facilities where floor space is at a premium. Despite its compact dimensions, the machine delivers full medium-to-large scale production capability. When comparing types of blow molding machine configurations on a floor-space-per-output basis, the EPA.ES-3C114 consistently demonstrates a strong advantage for cosmetic and daily chemical packaging producers worldwide.
6. Fully Automatic Operational Efficiency
As a fully automatic blow molding machine, the EPA.ES-3C114 eliminates the need for manual intervention at each production stage. From preform loading through bottle ejection, every step is automated and program-controlled. This full automation reduces reliance on skilled manual labor, minimizes human error in the production process, and enables consistent 24-hour operation with minimal operator supervision. For factories transitioning from semi-automatic or manual systems, the productivity gains are immediate and substantial. The automated blow molding machine process also enhances product consistency across large batch runs, a key quality requirement for cosmetic and daily chemical brands with strict packaging specifications and retailer quality audits.
How Does the EPA.ES-3C114 Fully Automatic Blow Molding Machine Work
Paso 1: Preparación de la materia prima
The blow molding machine process begins with thorough raw material preparation. PET, PETG, and compatible polymers undergo rigorous screening, blending, and moisture control before entering the production feed. For PET materials, pre-drying is critical to prevent hydrolytic degradation during processing. Strict incoming material quality control ensures that resin grade, viscosity, and contamination levels meet specification, setting the quality baseline for every bottle produced in the batch.
Paso 2: Moldeo por inyección de preformas
In the injection phase of the automatic PET blow molding machine process, selected and blended raw materials are fed into the injection system. After heating, melting, and plasticizing under precise temperature and pressure control, molten polymer is injected into the preform mold cavity. Parameters including melt temperature, injection pressure, hold time, and cooling duration are all servo-controlled to produce preforms with consistent wall thickness and accurate neck geometry for downstream blowing.
Paso 3: Realizar el precalentamiento
Following injection molding, preforms pass through a carefully calibrated infrared preheating tunnel. During this stage, the temperature of each preform is raised uniformly, with particular attention to the body wall thickness zone. The target is to achieve consistent plasticity and flexibility across all 74 preform positions simultaneously. Controlled preheating is critical for the two-stage blow molding machine process because uneven temperature distribution directly causes wall thickness variation and dimensional inconsistency in the finished bottles.
Paso 4: Moldeo por soplado y estiramiento
At the core of the injection stretch blow molding machine process, preheated preforms enter the 3-cavity blow mold. The stretch rod extends to biaxially orient the material longitudinally while high-pressure air at up to 35 kg/cm2 expands the preform radially against the mold cavity walls. This biaxial orientation significantly improves the mechanical strength, clarity, and barrier properties of the finished PET bottle. Precise servo control of stretch timing and air pressure profiles ensures consistent cavity-to-cavity quality across all three positions in every production cycle.
Applications of the EPA.ES-3C114 Daily Chemical Blow Molding Machine
Skincare and Serum Packaging
The EPA.ES-3C114 PET blow molding machine excels at producing premium skincare bottles including essences, serums, and facial toners. With neck diameter precision at 40mm and container heights reaching 330mm, it accommodates the slender, sophisticated bottle profiles that high-end cosmetic brands require. Superior wall thickness uniformity and crystal clarity in PET output meet the optical standards that retail shelf presence and brand premium positioning demand from modern cosmetic packaging lines worldwide.
Lotion and Cream Bottle Production
For moisturizer, body lotion, and facial cream containers, the machine's 95mm maximum body diameter and flexible cavity spacing accommodate the wide, round bottle formats popular in mass-market and professional cosmetic categories. The automatic blow molding machine process delivers smooth, blemish-free exterior surfaces that accept labeling, sleeve-shrink decoration, and direct screen printing without secondary surface treatment, reducing downstream finishing costs for high-volume daily chemical packaging manufacturers.
Shampoo and Hair Care Containers
Handling containers from 300ml to 1,500ml, the EPA.ES-3C114 daily chemical blow molding machine is ideally sized for shampoo, conditioner, hair mask, and scalp treatment bottles. Consistent neck finish at 40mm supports standard flip-top, disc-top, and pump closures used across the personal care sector. High production output at 2,400 bottles per hour enables cosmetic manufacturers to meet large retailer purchase orders and seasonal demand peaks without additional machine investment or extended production lead times.
Shower Gel and Body Wash Bottles
The machine's exceptional capability in producing irregularly shaped bottles makes it a strong fit for differentiating shower gel packaging. Brands increasingly use unique container geometry as a point-of-sale differentiation tool, and the EPA.ES-3C114 handles complex contoured shapes that challenge standard máquina de moldeo por soplado de plástico platforms. PETG material compatibility further expands design flexibility, allowing enhanced gloss, tinted transparency, and distinctive tactile surface textures that premium bath and body care brands increasingly specify in their packaging briefs.
Perfume and Fragrance Packaging
For fragrance secondary packaging and ancillary containers, the EPA.ES-3C114 delivers the dimensional accuracy and optical clarity that luxury fragrance presentation requires. The bottle blow molding machine produces containers with consistent clarity and precise neck finishes that interface reliably with crimped and threaded fine-mist spray closures. Its servo-controlled process minimizes batch-to-batch variation, an important capability for fragrance brands that maintain strict quality verification protocols for export shipments to European, North American, and Gulf market retailers.
Hand Care and Sanitizer Bottles
The EPA.ES-3C114 produces hand wash, hand cream, and hand sanitizer containers across the full 30ml to 1,500ml volume range. PET material compatibility provides the chemical resistance required for alcohol-based and surfactant-rich formulations used in hand hygiene products. The custom blow molding machine configuration options allow producers to customize bottle shape, shoulder geometry, and base design to match specific brand architecture or to produce private-label containers for multiple retail customers from a single mold set on the same machine platform.
Baby Care and Sensitive Skin Products
Baby shampoo, gentle body wash, and infant care product containers demand zero flash contamination and strict dimensional consistency. The EPA.ES-3C114, operating as a true fully automatic blow molding machine, eliminates manual handling at critical production stages and reduces particulate contamination risk. PETG options provide BPA-free clarity with superior impact resistance for the baby care segment. Clean production and high bottle-to-bottle consistency support quality certification requirements that major retailers and international baby care brands mandate for their approved supplier packaging programs.
Household Cleaning Product Containers
Household surface cleaners, fabric softeners, and dishwashing liquid bottles in the 500ml to 1,500ml segment are efficiently produced on this industrial blow molding machine platform. PET's excellent chemical resistance to common cleaning agents makes it the preferred material choice. The 2,400 bph output rate at 3 cavities ensures that household cleaning product manufacturers, who typically operate on thin margin economics requiring maximum production volume, can achieve the per-unit cost targets necessary to compete in mass retail and private-label cleaning product categories across both domestic and export markets.
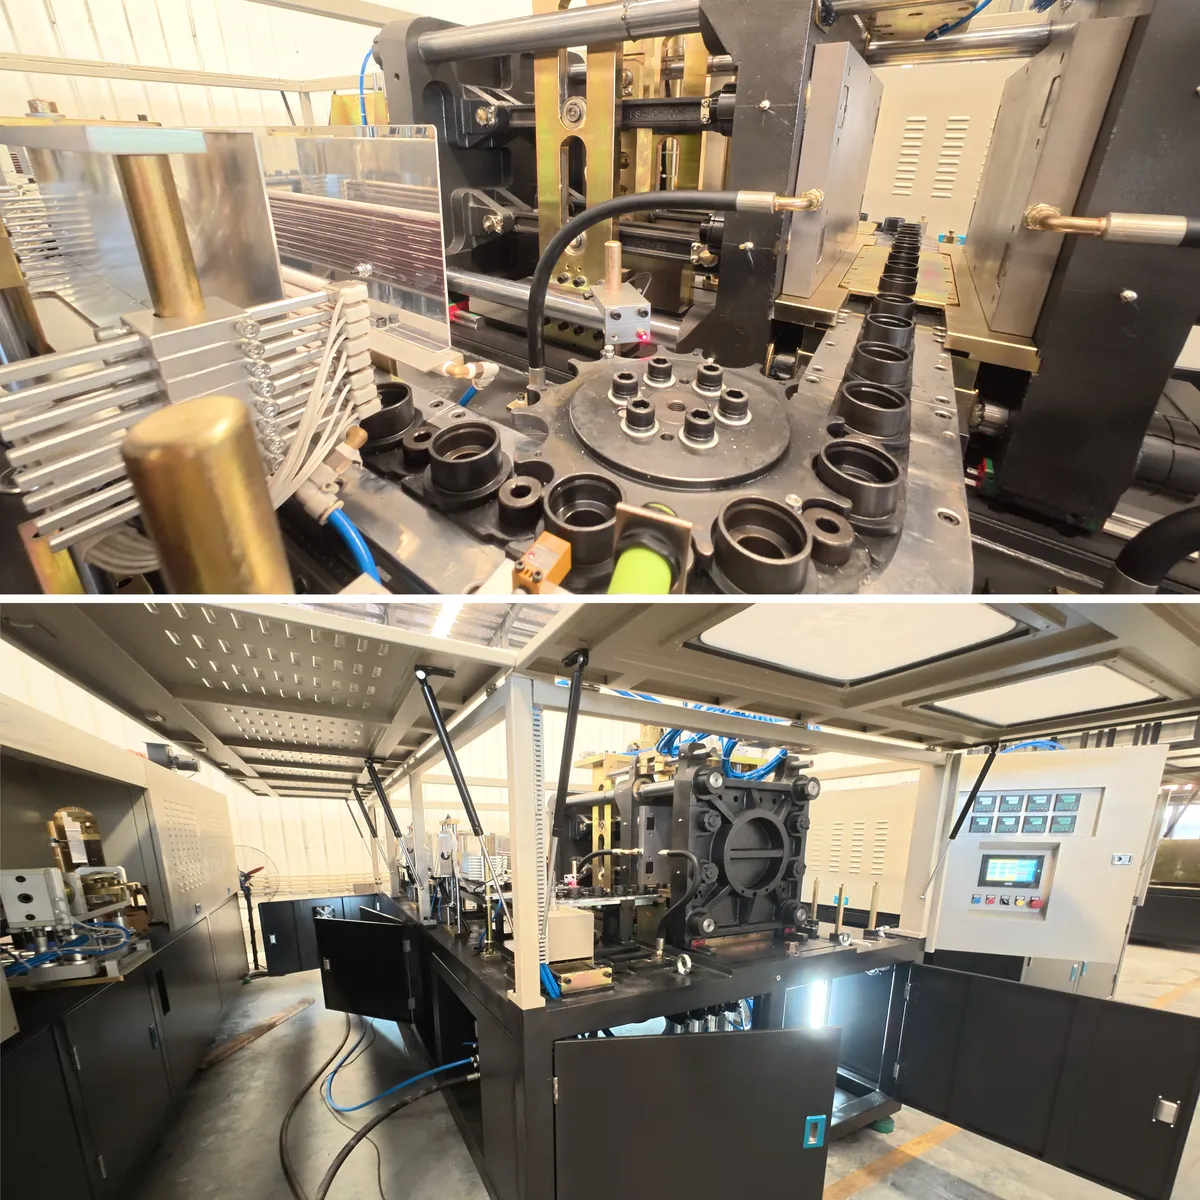
EPA.ES-3C114 PET Blow Molding Machine Parts
Feeding System
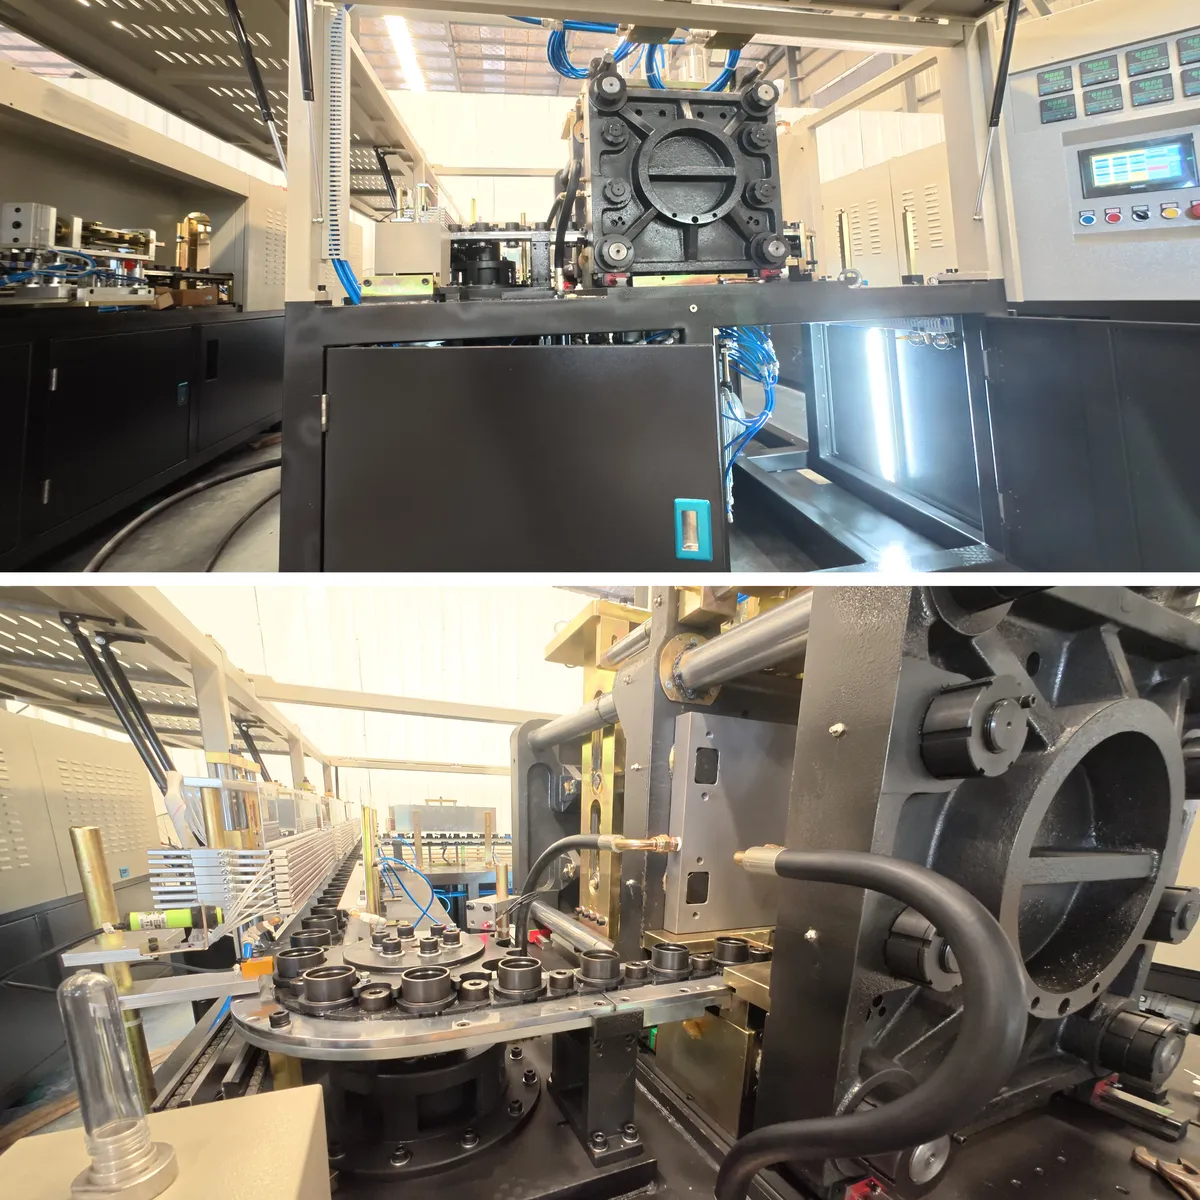
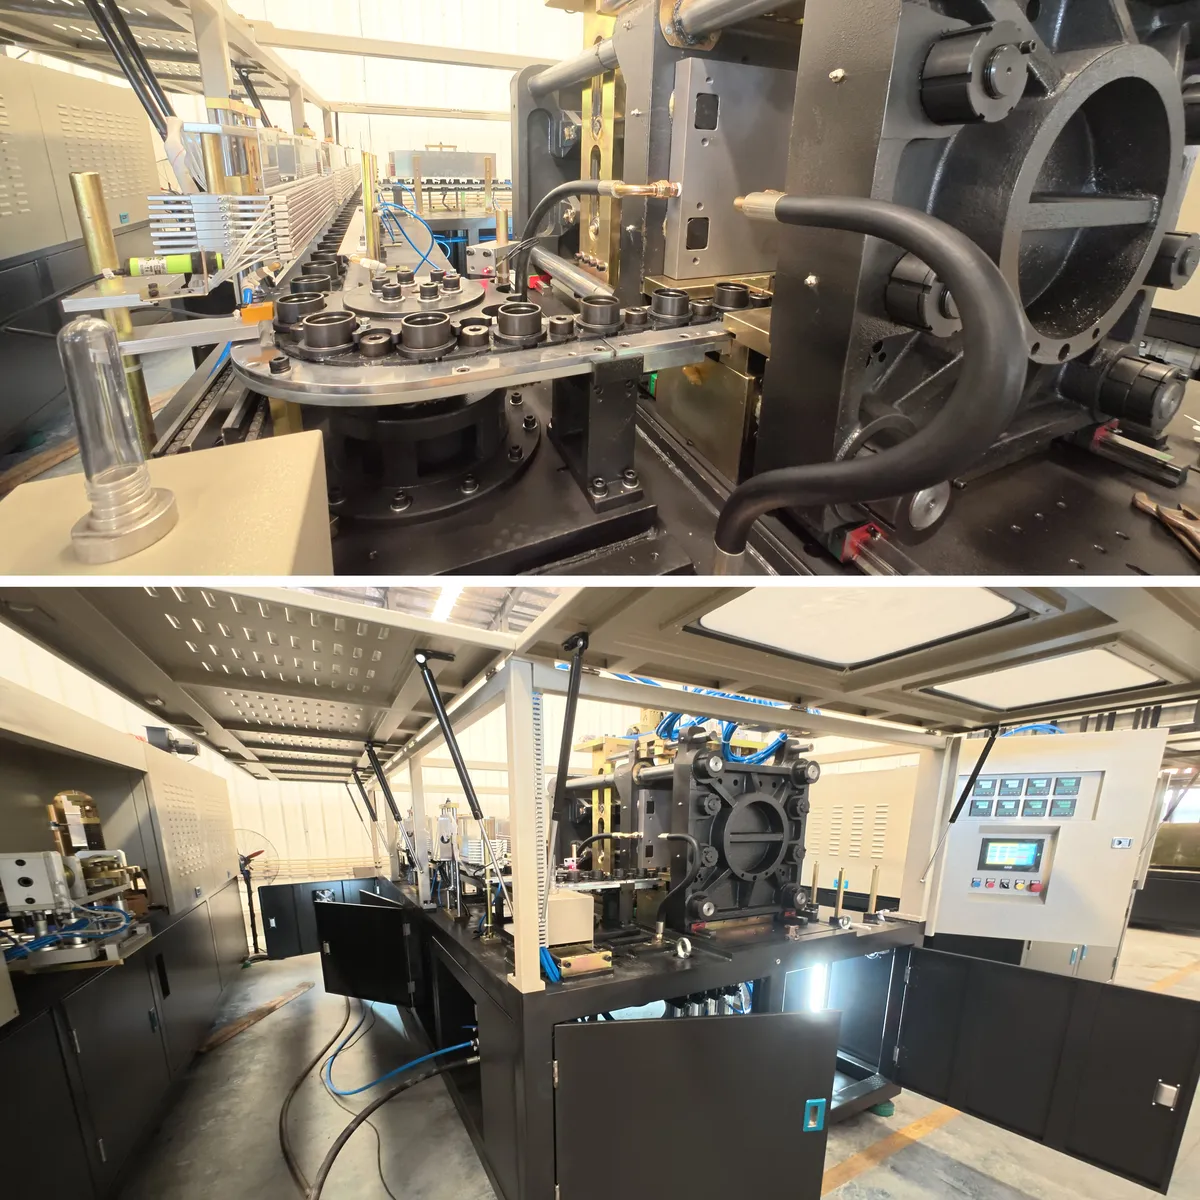
The feeding system comprises the hopper, preform conveyor, orientator, gravity rail, and associated steering and electric drive components. Raw PET preforms are fed into the blow molding machine through this fully automated loading path. The orientator aligns preforms correctly before they enter the conveying rail, ensuring consistent neck-up orientation for every preform entering the heating section. A reliable feeding system is fundamental to achieving the rated output of 2,400 bottles per hour without manual re-alignment or feeding interruptions during production shifts.
Preform Tilter
Because the EPA.ES-3C114 processes PET preforms, the preform tilter is a key blow molding machine part that automatically supplies pre-oriented preforms to the system hopper from bulk storage. The tilter handles the transition from randomly stacked bulk preforms to the single-file neck-up orientation required for the heating carousel. Its automated operation removes a manual labor step that can introduce inconsistency and injury risk in high-throughput production environments, contributing to the machine's suitability for continuous multi-shift operation.
Infrared Heating Section
The infrared heating section uses zoned quartz lamp arrays to raise preform temperatures uniformly to the blow-ready range. With a maximum heating power of 40kW and a working heating power of 18kW, the system delivers precise thermal profiles adjustable by zone and lamp intensity. The 74-position preform holder carousel ensures that all preforms reach identical temperature before entering the blow station. Independent zone adjustment allows operators to fine-tune temperature gradients for different bottle shapes, neck designs, and wall thickness profiles across the wide container range the machine supports.
Blow Mold Clamping Unit
The 3-cavity blow mold clamping unit secures the blow molds with a clamping stroke of 133mm and a mold-close distance of 114mm, providing the rigidity required to withstand 35 kg/cm2 blowing pressure without mold deflection. The precision mold alignment system ensures consistent parting-line quality and prevents flashing on finished bottles. Servo-driven mold closing delivers smooth, repeatable clamping force across every production cycle, which is critical for maintaining dimensional accuracy in complex-shaped cosmetic bottles where minor mold movement would cause unacceptable visual defects and functional failure at closure interfaces.
High-Pressure Air Compressor Station
The compressor station supplies both low-pressure operating air at 7 kg/cm2 and high-pressure blowing air at up to 35 kg/cm2. Low-pressure air consumption stands at 1,500 ltr/min while high-pressure consumption reaches 3,200 ltr/min at full production speed. The station integrates boosters, connectors, air tank, and pressure management controls. Stable air pressure supply directly determines bottle wall uniformity and dimensional accuracy in the bottle blow molding machine process, making compressor station sizing and reliability a critical specification factor for production engineers evaluating this equipment category.
Water Cooling System
The integrated water cooling system maintains mold temperature between 8 and 12 degrees Celsius at an operating pressure of 5 to 6 kg/cm2 with a flow rate of 30 ltr/min. Precise temperature control in the blow mold is fundamental to achieving rapid cycle times while producing dimensionally stable bottles. Inadequate cooling causes extended cycle times, bottle deformation, and inconsistent wall crystallinity. The EPA.ES-3C114's optimized cooling channel design ensures uniform mold temperature distribution across all three cavities, supporting both high output rates and consistent bottle quality across extended production runs.
Stretch Rod Assembly
The stretch rod assembly performs the biaxial orientation that gives PET bottles their characteristic strength, clarity, and barrier properties. With a stretching stroke of 350 to 450mm, the servo-controlled rods extend into each preform cavity simultaneously, orienting the polymer chains longitudinally before high-pressure air completes the radial blow. Precise stretch ratio control is essential for producing lightweight bottles with optimal wall thickness distribution. The EPA.ES-3C114's servo stretch system allows recipe-based parameter storage, enabling rapid mold changeovers between different bottle formats without manual adjustment calibration for each production run.
Bottle Exit Conveyor
The bottle exit conveyor transfers finished blown containers from the mold station to downstream filling or unscrambling systems. Designed to handle the full range of bottle shapes and sizes the machine produces, from small 30ml cosmetic bottles to 1,500ml daily chemical containers, the conveyor maintains bottle orientation and avoids scratching or marking the finished container surface. Its integration with downstream packaging lines supports seamless high-speed production at 2,400 bph, eliminating bottlenecks at the transition from blowing to filling that would otherwise limit the automatic blow molding machine's effective output in a complete packaging line configuration.
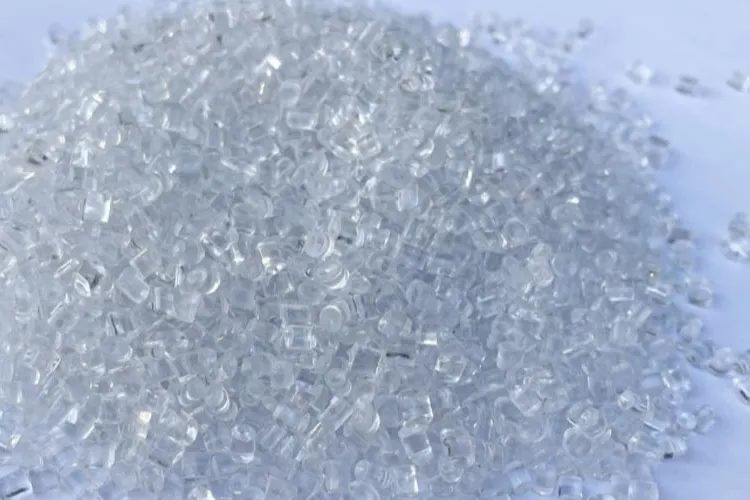
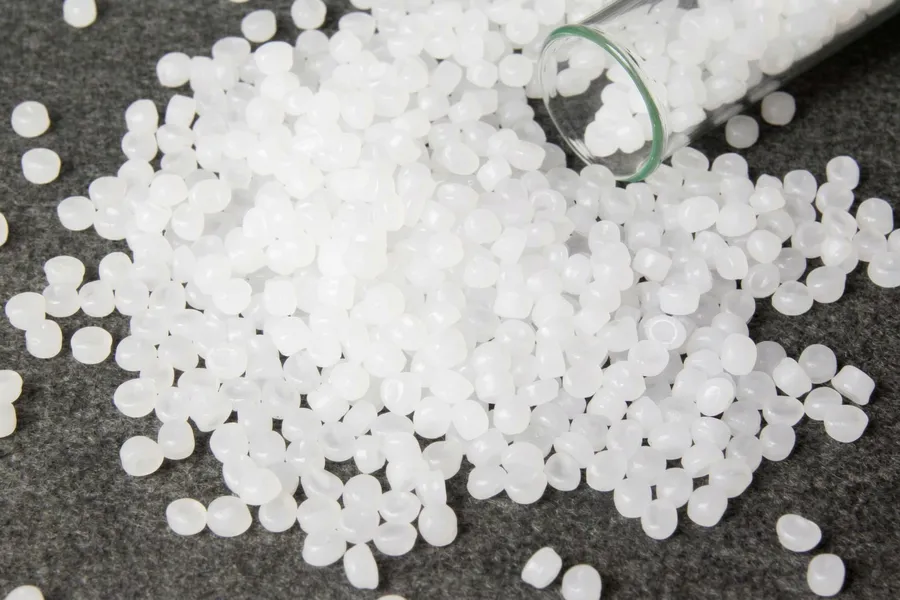
Materias primas compatibles
PP (polipropileno)
Polypropylene offers an excellent strength-to-weight ratio combined with good chemical resistance and a moderate processing temperature profile. It is particularly suited for daily chemical and cosmetic containers that require both flexibility and structural rigidity. PP's natural translucency and ability to accept colorants across the full spectrum makes it versatile for brand color programs. As a material option for the daily chemical blow molding machine, PP supports the production of refillable containers, dispensing bottles, and application-specific packaging with integrated functional elements like handles and grips.
PE (Polietileno)
Polyethylene, encompassing both LDPE and LLDPE grades, provides exceptional flexibility, moisture barrier properties, and ease of processing on this plastic blow molding machine. LDPE is widely used for squeeze bottles, travel-size containers, and flexible packaging formats in the cosmetic and personal care sectors. Its softness allows products to be dispensed by squeezing the container directly. LDPE bottles maintain flexibility even at low temperatures, making them suitable for cosmetic products sold in colder climate markets across Europe, North America, and East Asia.
PC (Policarbonato)
Polycarbonate delivers exceptional impact resistance and high-temperature tolerance that makes it suitable for reusable cosmetic containers, professional hair care packaging, and salon-grade product bottles that must withstand repeated use and sterilization cycles. PC's exceptional optical clarity rivals glass in finished container appearance, supporting premium brand positioning for luxury cosmetic lines. Where product formulations are compatible with PC chemistry, this material raises the perceived value of the packaging significantly, allowing cosmetic manufacturers to target higher retail price points with their finished product ranges.
PS (Polystyrene)
Polystyrene, particularly in its oriented form, provides good clarity and a smooth surface finish suitable for cosmetic and personal care containers in the value and mass-market segments. Its ease of processing and low material cost make PS an economical option for high-volume daily chemical packaging where transparency and reasonable surface quality are required but premium optical performance is not the primary specification. PS accepts printing and labeling readily, supporting the decoration requirements of mass-market cosmetic packaging produced in large volumes for retail chains and private-label programs.
PET (tereftalato de polietileno)
PET is the primary material for the EPA.ES-3C114 PET blow molding machine. Its combination of exceptional clarity, high strength, lightweight structure, and excellent gas barrier properties makes it the material of choice for premium cosmetic, personal care, and beverage bottles. PET produces bottles with a glass-like appearance that enhances product presentation on retail shelves. Its recyclability also supports sustainability objectives that cosmetic brands increasingly communicate to consumers as part of their product positioning and environmental responsibility programs.
PETG (tereftalato de polietileno glicol)
PETG is the preferred material for high-end cosmetic packaging requiring enhanced clarity, superior toughness, and greater design flexibility compared to standard PET. It processes at lower temperatures than PET, reducing thermal stress on the blow mold. PETG accepts metallic and tinted coloration more readily, supports deep embossing and unique tactile surface textures, and offers strong chemical resistance to alcohol-based cosmetic formulations. As a custom blow molding machine material option, PETG expands the range of premium packaging designs achievable on the EPA.ES-3C114 platform.
HDPE (Polietileno de Alta Densidad)
HDPE is widely used for opaque daily chemical bottles including laundry detergents, household cleaners, and personal care products where chemical resistance and container rigidity are the primary requirements. Its excellent resistance to temperature changes, acids, and bases makes it suitable for a broad range of cleaning product formulations. HDPE is also among the most widely recycled plastics globally, supporting regulatory compliance and brand sustainability programs in markets where extended producer responsibility legislation governs packaging material choices for daily chemical manufacturers.
PVC (Polyvinyl Chloride)
PVC is less commonly specified for new cosmetic packaging programs today due to evolving environmental regulations in major markets, but it remains in use for certain cleaning product containers where specific chemical resistance properties are required and where alternative materials do not meet formulation compatibility requirements. For buyers evaluating raw material options on their blow molding machine suppliers shortlist, PVC compatibility should be confirmed against local packaging regulations and retailer material restrictions before inclusion in a new product packaging specification program in key export markets.
 |
 |
 |
 |
 |
 |
Moldeo por inyección-soplado frente a moldeo por extrusión-soplado
Buyers evaluating blow molding machine manufacturers often face a foundational process selection decision: injection blow molding (IBM) or extrusion blow molding (EBM). Both processes create hollow plastic containers, but they form the starting shape in entirely different ways. Understanding this distinction is essential before specifying any automatic blow molding machine for a new production line.
Injection blow molding starts from an injection-molded preform. Molten plastic is injected around a core rod to form a precise preform and neck finish. The preform then moves to the blow station and is inflated inside the bottle mold. The finished bottle is removed without trimming flash. In British English the same process is often referenced as injection blow moulding.
Extrusion blow molding starts from a continuously extruded parison. The mold closes around the hollow tube and pinches off excess material. High-pressure air forms the bottle inside the mold, and flash must be trimmed after cooling. This process difference fundamentally affects neck precision, wall thickness control, trimming waste, and the type of container each process can produce economically.
| Característica | Moldeo por inyección-soplado (IBM) | Moldeo por extrusión-soplado (EBM) |
|---|---|---|
| Formulario inicial | Preforma moldeada por inyección | parsón extruido |
| Precisión del cuello | Extremely high; neck is pre-molded by injection | Standard; depends on mold closing and neck calibration |
| Chatarra / Residuos | Zero flash and very low process waste | Genera destellos que requieren recorte y reciclaje. |
| Mejor tamaño de contenedor | Small to medium precision bottles (30ml to 1,500ml) | Medium to large hollow containers and industrial parts |
| Costo del moho | Higher upfront investment for precision tooling | Lower initial mold costs for large hollow containers |
| Mejores aplicaciones | Pharmaceutical, cosmetic, lab, medical packaging | Jerry cans, drums, tanks, large industrial containers |
| Prioridad de calidad | Consistencia dimensional y fiabilidad del sellado | Flexibilidad de tamaño y economía del volumen de contenedores |
¿Cuándo elegir el moldeo por inyección-soplado?
- Small and medium precision bottles with accurate threaded necks
- Pharmaceutical, medical, cosmetic, laboratory, or high-value packaging applications
- Production environments requiring zero flash waste and clean operation without secondary trimming
- Applications demanding stable bottle dimensions, repeatable wall thickness, and reliable closure sealing
- PET and PETG bottle production for cosmetic and daily chemical packaging
When to Choose Extrusion Blow Molding
- Large bottles, jerry cans, drums, tanks, and complex hollow industrial parts
- Applications where lower tooling cost is a priority over highest neck precision
- Wide product geometry variety including handled containers and asymmetric shapes
- Applications where trimming flash is an acceptable part of the production process
Cost Perspective: EBM equipment can carry a lower initial purchase price for large containers, but the total production cost calculation must also include resin loss from flash trimming, secondary labor, reject rates, and downstream handling. For precision cosmetic bottles where IBM reduces waste and quality risk, the total cost of ownership over a multi-year production period often favors the IBM process even when initial machine and mold investment is higher. For large industrial containers, EBM typically remains the more economical process choice. Materials used across both processes include HDPE, PP, LDPE, PET, PETG, and PVC, with material choice always validated against bottle geometry, regulatory requirements, and sealing specifications.
Características del molde de la máquina de moldeo por soplado de botellas cosméticas
Molde de inyección de preformas
- The two-part die lip design guarantees coaxial alignment between the preform and the neck finish during every injection cycle, eliminating the neck eccentricity that causes closure sealing failures in finished bottles.
- Optimized cooling water channel geometry improves preform cooling efficiency and ensures rapid cycle times without compromising dimensional stability in the cooled preform wall.
- Preform-forming components use imported 2316 die steel, which is inherently rust-resistant and has undergone heat treatment to achieve the hardness and dimensional stability required for precision cosmetic bottle neck production.
- Core plate, cavity plate, and other structural components use 420 stainless steel, providing excellent corrosion resistance in the humid, temperature-cycled environment of continuous injection mold operation.
- The maintenance-accessible design reduces mold servicing time during scheduled maintenance intervals, minimizing production downtime on this blow molding machine platform.
- Standard interchangeable die fittings across the mold range reduce spare parts inventory requirements and allow cross-utilization of components between compatible mold sets.
- Advanced modular mold design allows a single mold set to produce more than one preform variant, increasing tooling investment efficiency for manufacturers with multiple bottle SKUs.
Moldeo por soplado
- Blow mold bodies are manufactured from high-quality steel selected for its thermal conductivity, machinability, and resistance to the fatigue stresses generated by repeated high-pressure blowing cycles at 35 kg/cm2.
- All plastic bottle cavity geometries are designed using advanced 3D CAD and simulation software, ensuring that cavity shapes achieve the target wall thickness distribution before the first physical mold is cut.
- A broad range of standard and custom bottle designs is available for selection, allowing buyers to start production with proven cavity geometries while specifying custom cavities for proprietary bottle shapes.
- Cooling water channels within the blow mold body are designed to deliver uniform temperature distribution across the entire cavity surface, preventing hot spots that cause uneven crystallinity and dimensional variation in finished bottles.
- All structural metal components in the blow mold assembly are machined on CNC machining centers, ensuring dimensional accuracy and surface finish consistency that would not be achievable with conventional machining methods for precision cosmetic bottle blow molding machine tooling.
- Mold parting surface precision and surface texture are optimized to minimize parting line marks on finished bottle exterior surfaces, reducing secondary cosmetic rejection rates for premium cosmetic packaging production runs.
 |
 |
EPA.ES-3C114 Plastic Blow Molding Machine Operating Precautions
1. Pre-Startup Inspection Protocol
Before every production startup, operators must conduct a systematic inspection of all mechanical connections, lubrication points, and fastener torque levels. Verify that cooling water supply is active and within the specified 5 to 6 kg/cm2 pressure range and 8 to 12 degree Celsius temperature range. Confirm that air supply lines are secure and that both low-pressure and high-pressure systems are functioning correctly. Check electrical panel indicators for any fault codes from the previous production session before initiating the startup sequence. This pre-startup routine prevents equipment damage and ensures operator safety on the fully automatic blow molding machine.
2. Preform Quality and Material Verification
Only use PET or PETG preforms that meet the specifications confirmed during mold qualification testing. Verify preform weight, IV (intrinsic viscosity), moisture content (maximum 50 ppm for PET), and dimensional consistency before loading each new batch. Using out-of-specification preforms is the single most common cause of bottle defects, burst failures in the blow station, and mold damage in a PET bottle blow molding machine. Pre-dry all PET preforms at 160 to 180 degrees Celsius for a minimum of 4 hours to prevent hydrolytic degradation during processing, which permanently reduces polymer molecular weight and compromises finished bottle mechanical properties.
3. Temperature Parameter Management
Heating zone temperatures must be set and verified against the approved process parameter sheet for each bottle format and preform design. Never override automatic temperature safeguards or run the blow molding machine with heating zones that have not reached setpoint temperature. Overheated preforms cause premature crystallization and whitening; underheated preforms cause burst failures in the blow station or produce bottles with unacceptable wall thickness distribution. Record heating zone setpoints and actual temperatures at the start of each production run as part of the batch quality documentation required for cosmetic manufacturing compliance programs.
4. Air Pressure System Safety
The EPA.ES-3C114 operates with blowing pressures up to 35 kg/cm2, which represents a significant stored energy hazard. All personnel must maintain safe distances from the blow station during active production. Never attempt to open the blow mold manually during a cycle or insert tools into the mold area while the machine is running. Verify pressure relief valves are functional and set to the correct relief pressure before startup. Inspect all high-pressure air hoses, fittings, and connections for wear, cracking, or leakage on a daily basis, and replace any components showing deterioration immediately to prevent pressure release incidents on the production floor.
5. Mold Changeover Procedures
Mold changeovers on the EPA.ES-3C114 must be performed following the documented lockout-tagout energy isolation procedure. Allow the blow mold to cool to below 40 degrees Celsius before handling. Use the correct lifting tools and personnel team size specified in the maintenance manual for mold weights. After installing a new mold, verify that all cooling water connections are secure and leak-free before initiating a trial cycle. Run a slow-speed trial sequence and inspect the first 20 bottles from each cavity before releasing to full production speed. Document changeover completion time and first-article inspection results in the production log as part of the blow molding machine process quality record.
6. Routine Maintenance and Lubrication Schedule
Follow the manufacturer-prescribed lubrication schedule for all guide rails, cam tracks, stretch rod linear bearings, and preform transfer mechanisms. Use only the specified lubricant grades to avoid contaminating product contact surfaces or causing accelerated component wear. Clean heating lamps and reflector surfaces at the scheduled interval to maintain heating efficiency and prevent uneven preform temperature profiles. Replace worn seals, O-rings, and blow valve components at the intervals specified in the maintenance schedule rather than waiting for visible failure. Proactive maintenance on this industrial blow molding machine significantly extends component life and prevents unplanned production stoppages that generate disproportionate costs in high-output packaging operations.
How to Select the Right Blow Molding Machine
1. Define Your Container Volume Range
The first specification parameter for any blow molding machine selection is the target container volume range. The EPA.ES-3C114 covers 30ml to 1,500ml, making it ideal for cosmetic and personal care bottles. If your product range extends to 5,000ml or beyond, consider models in the 4-cavity series or food jar category from the Ever-Power range. Matching machine container capacity to your product portfolio ensures that you are not running an oversized machine at reduced efficiency or attempting to produce containers outside the equipment's design parameters, both of which increase per-unit production costs and quality risk.
2. Match Cavity Count to Output Requirements
Cavity count directly determines the output rate of any automatic blow molding machine. The EPA.ES-3C114's 3-cavity configuration delivers 2,400 bph at rated speed. Calculate your required annual output, account for planned downtime and changeover hours, and work backward to determine the minimum cavity count and machine speed that meets your production plan. If output requirements significantly exceed this model's rated capacity, evaluate the 4-cavity and 6-cavity models from the same product series. Over-specifying cavity count increases capital cost without proportional operational benefit for smaller production volumes.
3. Confirm Material and Process Compatibility
Verify that the blow molding machine suppliers you are evaluating can confirm compatibility between the machine and your specific resin grades. The EPA.ES-3C114 is designed and validated for PET and PETG, which cover the vast majority of cosmetic and daily chemical packaging applications. If your product requires PP, HDPE, or specialty engineering resins, evaluate whether the machine's heating system and process parameters support those materials. Material incompatibility discovered after purchase is an expensive problem that requires either accepting suboptimal bottle quality or investing in machine modifications that may not be technically feasible.
4. Evaluate Bottle Shape Complexity
Evaluate whether your target bottle shapes require standard cylindrical geometry or complex irregular profiles. Not all plastic blow molding machine platforms handle high-complexity shapes equally. The EPA.ES-3C114 is specifically engineered for complex, irregularly shaped cosmetic bottles that challenge standard equipment. If your product portfolio includes unique contoured bottles, oval cross-sections, deep grip recesses, or complex shoulder geometries, confirm that the supplier has produced similar shapes on the specific machine model you are evaluating, and request sample bottles and technical validation data before committing to a purchase decision.
5. Assess Energy Consumption and Operating Cost
The total cost of machine ownership over a five to ten year production life includes purchase price, installation, tooling, maintenance, and electricity consumption. Servo-driven fully automatic blow molding machine platforms like the EPA.ES-3C114, with 18kW working heating power versus the 40kW maximum, offer significant energy efficiency advantages over older hydraulic systems. Request energy consumption data at rated output for each machine you evaluate and model the 5-year electricity cost at your facility's local energy tariff. Energy cost difference between machine generations often exceeds the initial purchase price premium of newer servo-driven equipment in high-utilization production environments.
6. Evaluar el servicio posventa y la disponibilidad de repuestos.
For any industrial blow molding machine investment, after-sales support capability is as important as machine performance specifications. Verify that the supplier maintains spare parts inventory for critical wear components including blow valves, stretch rods, preform holders, heating lamps, and drive belts. Confirm maximum committed response time for technical support and on-site service for your region. Evaluate the completeness and language quality of the machine manual and process setup documentation. A machine that produces well but loses two weeks of production awaiting spare parts delivers a much lower return on investment than the initial purchase cost calculation suggested.
¿Por qué elegir la máquina de moldeo por soplado de PET de Ever-Power?
Mexico Ever-Power ISBM Machinery Co., Ltd is a specialist company dedicated to the research and development, production, sales, and international trade of fully automatic blow molding machines. Our product range encompasses injection blow molding machines, extrusion blow molding machines, injection stretch blow molding machines, and auxiliary machinery, giving buyers a complete solution source for any hollow plastic container manufacturing requirement.
Ever-Power maintains an excellent R&D team that brings together experienced engineers and technical personnel who have spent their careers specializing in injection-blowing machinery and injection-blowing mold development. With deep theoretical knowledge and extensive practical experience across hundreds of production deployments, our technical team provides the detailed, application-specific guidance that generic blow molding machine manufacturers cannot match. We deliver thorough pre-sale technical consultation, responsive in-sale support, and committed after-sale service to every customer globally.
Our product applications cover pharmaceutical packaging, food packaging, health care packaging, and cosmetic packaging, encompassing all major plastic packaging categories. We produce and support equipment capable of handling HDPE, LDPE, PET, PETG, PP, PS, PPSU, PC, Tritan, ABS, PLA, environmental corn materials, EVA, PCTG, and other specialty resins across container volumes from 1ml to 1,000ml and beyond. This breadth of material and application expertise means that regardless of your product category or packaging specification, Ever-Power has the technical knowledge to advise you on the optimal machine configuration for your requirements.
Ever-Power se rige por los principios de desarrollo empresarial de autosuficiencia, integridad, pragmatismo, innovación y responsabilidad. Desarrollamos proyectos integrales llave en mano para producir productos de moldeo por inyección-soplado de alta gama que cumplen con los estándares de calidad que exigen nuestros clientes, con una calidad y consistencia de fabricación que nos permite establecer alianzas duraderas con fabricantes de envases para cosméticos, productos farmacéuticos, alimentos y productos químicos de uso diario en todo el mundo. La colaboración con marcas reconocidas a nivel mundial, como C'ESTBON, Haitian, Luhua, Walch, Blue Moon, PROYA, Liby, Estee Lauder, Walmart, Dasenlin y Shanliang Eye Drops, confirma el nivel de calidad que Ever-Power ofrece como socio proveedor de máquinas de moldeo por soplado comprometido a largo plazo.
 |
 |
 |
 |
 |
 |
Preguntas frecuentes
P: ¿Cuál es el tamaño máximo de botella que puede producir la máquina de moldeo por soplado EPA.ES-3C114?
A: La EPA.ES-3C114 produce envases de hasta 1500 ml, con un diámetro máximo de 95 mm y una altura máxima de 250 mm en configuración estándar o de 330 mm con la opción de carrera de estiramiento extendida. El diámetro del cuello es de hasta 40 mm, compatible con los cierres estándar utilizados en envases de cosméticos y productos químicos de uso diario. Para envases de más de 1500 ml, los modelos de 4 cavidades o multicavidades de la misma serie Ever-Power cubren volúmenes de hasta 15 000 ml o más, según la selección y configuración del modelo.
P: ¿Qué materiales puede procesar la máquina de moldeo por soplado automática EPA.ES-3C114?
A: El modelo EPA.ES-3C114 está diseñado y optimizado específicamente para materiales PET y PETG, las resinas predominantes en la producción de envases para cosméticos y productos químicos de uso diario. El PET ofrece una claridad, resistencia y propiedades de barrera excepcionales para envases cosméticos de alta gama. El PETG ofrece mayor flexibilidad de diseño, una resistencia superior y una excelente compatibilidad con colorantes metálicos y tintados para marcas de cosméticos de lujo. Si su aplicación requiere PP, HDPE u otras resinas no incluidas en esta lista, póngase en contacto con nuestro equipo técnico para consultar modelos alternativos de la gama Ever-Power que se ajusten mejor a sus necesidades específicas de materiales y diseños de envases.
P: ¿Cuál es la producción real de la máquina de moldeo por soplado de botellas de PET EPA.ES-3C114 en condiciones de fabricación reales?
A: La producción teórica nominal es de 2400 botellas por hora en 3 cavidades. En condiciones de fabricación reales, la producción real suele oscilar entre 90% y 97% de la capacidad nominal, dependiendo de la consistencia de la calidad de la preforma, la complejidad de la forma de la botella, el grado de resina y las condiciones ambientales. Los comentarios de los clientes indican consistentemente una producción sostenida de entre 2250 y 2380 botellas por hora en instalaciones bien mantenidas con suministro de preformas de calidad controlada. Se recomienda incorporar un margen de eficiencia de 5% a 10% al calcular la capacidad de producción anual para fines de planificación de la fábrica, a fin de realizar un modelado financiero conservador de la inversión en la máquina.
P: ¿Qué capacidad de compresor de aire se requiere para la máquina de moldeo por soplado automática EPA.ES-3C114?
A: La norma EPA.ES-3C114 requiere un suministro de aire a baja presión de 7 kg/cm² con un consumo de 1500 l/min, y un suministro de aire de soplado a alta presión de 35 kg/cm² con un consumo de 3200 l/min. El dimensionamiento del compresor debe incluir un margen de al menos 20% por encima de estas cifras de consumo nominal para tener en cuenta las caídas de presión en las tuberías de distribución y para gestionar los picos de demanda de arranque sin que la estación de soplado se quede sin suministro. Para la mayoría de las instalaciones, se recomienda un sistema de compresor de refuerzo de alta presión dedicado junto con el suministro de aire de baja presión de la instalación. Nuestro equipo técnico puede proporcionar orientación específica sobre el dimensionamiento del compresor en función de la configuración de las tuberías de su instalación y la infraestructura de aire comprimido existente.
P: ¿Cuánto tiempo tarda la instalación y puesta en marcha de la máquina de moldeo por soplado EPA.ES-3C114?
A: El plazo típico de instalación y puesta en marcha del EPA.ES-3C114 oscila entre 5 y 10 días hábiles, dependiendo de la preparación de las instalaciones, la disponibilidad de los servicios públicos y si los moldes están precalificados o requieren ajustes in situ. Las instalaciones que cuentan con todos los servicios públicos, incluyendo aire comprimido, agua de refrigeración y suministro eléctrico, puestos en marcha antes de la llegada de la máquina, y que disponen de operadores a tiempo completo durante la puesta en marcha, suelen alcanzar el plazo más corto. Ever-Power proporciona asistencia para la puesta en marcha y documentación de capacitación para operadores, lo que facilita un proceso de arranque exhaustivo. Además, se ofrece asistencia técnica remota durante todo el período de puesta en marcha para las instalaciones donde la asistencia in situ no está incluida en el paquete de compra.
P: ¿Puede la máquina de moldeo por soplado de botellas de cosméticos EPA.ES-3C114 producir botellas con formas irregulares?
A: Sí, la producción de botellas complejas y de formas irregulares es una de las principales ventajas de diseño de la plataforma EPA.ES-3C114 y se destaca explícitamente en sus especificaciones. El sistema de varilla de estiramiento con servocontrol, la gestión precisa de la presión de soplado y el control estable de la temperatura del agua de refrigeración permiten la producción consistente de botellas con geometrías no cilíndricas, incluyendo secciones transversales ovaladas, formas asimétricas, hendiduras de agarre profundas y cuerpos contorneados que representan un desafío para equipos menos capaces. Varios clientes han confirmado esta capacidad con botellas cuyas formas no se lograron producir con éxito en máquinas de la competencia. Para validar un diseño de botella complejo específico, recomendamos enviar el dibujo de la botella para su revisión técnica antes de confirmar la compra.
P: ¿Cuál es el tiempo típico de cambio de molde en la máquina de moldeo por soplado EPA.ES-3C114?
A: Los operadores experimentados suelen completar un cambio de molde completo en la EPA.ES-3C114, incluyendo la extracción del molde de soplado, la instalación del nuevo molde, la reconexión del agua de refrigeración, la carga de parámetros y la inspección del primer artículo, en 2 a 4 horas. El primer cambio en un nuevo diseño de molde puede requerir tiempo adicional para la optimización inicial de parámetros. Las instalaciones que mantienen un almacenamiento organizado de moldes con recetas de parámetros predocumentadas para cada formato de botella, y que utilizan la función de almacenamiento de recetas de la máquina, logran consistentemente tiempos de cambio en el extremo inferior de este rango. Se recomienda capacitación específica para el cambio de molde y documentos de procedimiento estandarizados para las instalaciones que realizan cambios frecuentes de formato en líneas de envasado de cosméticos y productos químicos de uso diario.
P: ¿Qué certificaciones y estándares de calidad cumple la máquina de moldeo por soplado EPA.ES-3C114?
A: La EPA.ES-3C114, fabricada sobre la plataforma de Ever-Power Machinery, cumple con los estándares internacionales de calidad. Ever-Power Machinery posee múltiples patentes nacionales de modelos de utilidad y ha recibido la certificación CE para los modelos relevantes de su gama de productos, como se muestra en la documentación del certificado de cualificación de la empresa. Para compradores en mercados regulados que requieren certificaciones o documentación de seguridad específicas para la importación, póngase en contacto con nuestro equipo de ventas para solicitar el paquete de documentación de certificación vigente aplicable a la EPA.ES-3C114 y confirmar qué certificaciones son relevantes para los requisitos reglamentarios de su mercado de destino en materia de importación de máquinas de moldeo por soplado industrial.
P: ¿Cómo se compara la EPA.ES-3C114 con otros tipos de máquinas de moldeo por soplado para envases de cosméticos?
A: Entre los principales tipos de máquinas de moldeo por soplado utilizadas para el envasado de cosméticos, la EPA.ES-3C114 es una máquina de moldeo por soplado e inyección de dos etapas (ISBM), que produce la mayor claridad de botella, precisión del cuello y consistencia del espesor de pared alcanzables en la producción automatizada de botellas. En comparación con las máquinas de moldeo por soplado y extrusión (EBM), produce cero desperdicio de rebabas y una precisión superior en el acabado del cuello. En comparación con las máquinas de moldeo por soplado e inyección de una etapa (IBM), la arquitectura de dos etapas permite una mejor optimización de la temperatura de la preforma y admite mayores tasas de producción para volúmenes de producción en el rango de cosméticos y productos químicos de uso diario. Para las marcas que requieren botellas cosméticas de PET o PETG transparentes de primera calidad con un rendimiento de cierre preciso, la plataforma de soplado y estiramiento de dos etapas supera consistentemente a las alternativas en calidad general del envase y eficiencia de producción.
P: ¿Qué repuestos debo tener en stock para la máquina de moldeo por soplado EPA.ES-3C114?
A: El inventario recomendado de repuestos en planta para la EPA.ES-3C114 incluye lámparas de calentamiento infrarrojo para todas las zonas de calentamiento, sellos y juntas tóricas para válvulas de soplado, puntas de varillas de estiramiento, husillos de soporte de preformas, elementos de filtro de aire para sistemas de baja y alta presión, electroválvulas de agua de refrigeración y los tamaños de fusibles más comunes para servomotores y PLC. Disponer de estos componentes de desgaste rápido y alta importancia permite a su equipo de mantenimiento resolver las interrupciones de producción más comunes sin tener que esperar la entrega internacional de repuestos. Nuestro equipo técnico puede proporcionarle una lista de repuestos recomendada específica para la EPA.ES-3C114, basada en su volumen de producción anual previsto y su patrón de turnos al adquirir la máquina.
Opiniones de clientes
Rajesh Patel, Industria Química Diaria, India
"En general, es una buena máquina. Compramos el modelo ES-3C114 para nuestra línea de embotellado de champú en Mumbai el año pasado. La producción se ha mantenido constante entre 2300 y 2350 botellas por hora en nuestras condiciones, muy cerca de las 2400 nominales. El consumo de energía es notablemente menor que con nuestra máquina anterior, lo cual era importante dado el elevado coste de la electricidad aquí. Lo único que diría es que la comunicación previa a la venta podría ser más rápida en ocasiones, pero el equipo técnico posterior a la compra ha respondido con prontitud a todas nuestras preguntas. Los repuestos que pedimos llegaron en dos semanas, lo cual es aceptable para nuestra planificación. Sin duda, consideraremos Ever-Power para nuestra próxima máquina cuando ampliemos la línea."
Ana Carvalho, Industria del Envasado de Cosméticos, Brasil
"En nuestra planta a las afueras de São Paulo, operamos tres de estas máquinas para producir envases de cosméticos para varias marcas de belleza brasileñas. Elegimos Ever-Power por su reputación en el manejo de envases con formas irregulares, y sin duda han cumplido con creces. Producimos un tipo específico de envase de suero con sección transversal ovalada que otras dos marcas de máquinas que probamos no pudieron procesar, pero la ES-3C114 lo produce de forma consistente sin necesidad de ajustes significativos tras la configuración inicial. El control de la temperatura del agua de refrigeración es muy estable, lo que facilita enormemente el manejo de la forma irregular. Estamos muy satisfechos tras 14 meses de funcionamiento. Nuestro índice de rechazo de calidad es inferior a 1,2%, el mejor resultado que hemos obtenido con cualquier equipo para este tipo de envase."
Budi Santoso, embalajes para el cuidado personal, Indonesia
La coordinación logística del envío fue impecable. Nos preocupaba el plazo de entrega a nuestra planta en Yakarta, dado el peso de la máquina (4000 kg), pero la documentación de exportación estaba completa y era precisa, y la máquina llegó a tiempo, dentro del plazo acordado. La instalación se realizó sin problemas gracias al soporte técnico remoto proporcionado durante la puesta en marcha. Llevamos unos seis meses fabricando botellas de gel de ducha de 300 ml en PETG y la claridad que obtenemos es excelente. De hecho, nuestro cliente minorista comentó positivamente la mejora en el aspecto de la botella en comparación con nuestro proveedor anterior. La recomendación de un rango de temperatura del agua de refrigeración de 8 a 12 grados fue perfecta para nuestras condiciones de producción de PETG.
Miguel Torres, Industria de Envases Cosméticos, México
Evaluamos a cuatro proveedores de máquinas de moldeo por soplado antes de seleccionar Ever-Power para nuestra nueva línea de envasado de cosméticos en nuestra planta cerca de la Ciudad de México. La EPA.ES-3C114 tenía un precio competitivo, pero lo que realmente diferenció a Ever-Power fue la respuesta del soporte técnico durante nuestro proceso de evaluación. Nos proporcionaron recomendaciones detalladas sobre los parámetros del proceso para nuestro grado específico de PET antes de la compra, lo que nos dio la confianza de que realmente comprendían nuestra aplicación. Llevamos cinco meses operando y produciendo botellas de loción de 150 ml a 800 ml, y el cambio entre formatos de botella es sencillo una vez que se guardan las recetas de parámetros. El equipo de mantenimiento encontró la máquina fácil de operar, lo cual es importante para el flujo de trabajo de nuestro equipo de servicio durante las paradas programadas.
Nguyen Thi Lan, Industria de Envases por Contrato, Vietnam
"Gestionamos una planta de fabricación por contrato de envases para productos de cuidado personal de tamaño mediano cerca de Hanói, y hace unos diez meses incorporamos la EPA.ES-3C114 como tercera máquina a nuestra línea de producción de botellas cosméticas. Sinceramente, la calidad de la máquina ha sido similar a la de nuestras dos primeras unidades Ever-Power, que llevamos tres años utilizando sin mayores problemas. El sistema de servoaccionamiento es notablemente más silencioso que el de las máquinas hidráulicas antiguas que utilizábamos, lo que mejora las condiciones de trabajo de los operarios. Algo que nos impresionó fue la estabilidad de la zona de calentamiento. Trabajamos en turnos de 16 horas y la temperatura se mantiene constante durante todo el turno, lo que reduce directamente la frecuencia de muestreo de calidad y libera tiempo para el control de calidad. Una excelente relación calidad-precio."
Chen Wei, Industria del Envasado de Cosméticos, China
Llevamos unos ocho meses utilizando la EPA.ES-3C114 en nuestra planta de envasado de cosméticos en Guangzhou y, sinceramente, ha sido una de las mejores decisiones que hemos tomado en cuanto a equipamiento últimamente. Producimos principalmente botellas de tónico y loción de PET de 200 ml a 500 ml, y la consistencia entre botellas ha sido excelente. La precisión del acabado del cuello es especialmente importante para nosotros, ya que utilizamos tapones de bomba con tolerancias muy estrictas, y prácticamente no hemos tenido ningún rechazo por fugas en los tapones desde su instalación. La configuración de la máquina se completó en unos cinco días, incluyendo la formación del operario, y la documentación proporcionada fue lo suficientemente completa como para que nuestros ingenieros pudieran realizar la mayoría de los ajustes de parámetros de forma independiente.
Mehmet Yilmaz, Envases Cosméticos Premium, Turquía
Fabricamos envases de alta gama para productos de cuidado de la piel para varias marcas de belleza europeas y nacionales desde nuestra planta en Estambul. La decisión de adquirir la EPA.ES-3C114 se basó principalmente en su capacidad para procesar botellas de formas irregulares, que nuestros clientes europeos solicitan cada vez más para diferenciar sus productos premium. La máquina ha procesado sin problemas todas las formas complejas que le hemos presentado en 12 diseños de botellas diferentes durante nueve meses de producción. La respuesta del servicio de atención al cliente cuando tuvimos un problema inicial con el sensor de la zona de calentamiento fue rápida y la pieza de repuesto llegó en nueve días hábiles, incluyendo el despacho de aduanas, lo cual consideramos aceptable dado el envío internacional desde México. En general, es una máquina fiable para nuestra categoría de aplicación.
Sipho Dlamini, envasado diario de productos químicos, Sudáfrica
"Llevamos casi un año utilizando esta máquina en nuestra planta de la provincia de Gauteng para la producción diaria de botellas de productos químicos. Sus dimensiones de 3240 x 1800 mm se ajustan perfectamente al espacio disponible, lo cual era un factor clave en el diseño de nuestras instalaciones. La producción se ha mantenido constante en torno a las 2380 botellas por hora para nuestro formato de botella de jabón líquido de 200 ml. Inicialmente, teníamos algunas dudas sobre el dimensionamiento del compresor de aire para un consumo de alta presión de 3200 l/min, y el equipo técnico nos brindó una orientación clara que nos ayudó a dimensionar correctamente nuestra inversión en el compresor. El sistema de refrigeración ha funcionado sin problemas en todo momento, lo cual es importante porque la temperatura ambiente aquí puede suponer un desafío para los sistemas de refrigeración por agua durante los meses de verano. Un rendimiento sólido para nuestras necesidades de producción."
María Santos, Envases para el cuidado personal, Filipinas
Fabricamos botellas de productos de cuidado personal de marca propia para varias cadenas de supermercados del sudeste asiático desde nuestra fábrica en Manila. Adquirimos la EPA.ES-3C114 hace siete meses para reemplazar equipos obsoletos y la mejora en la productividad ha sido sustancial. Nuestra máquina anterior producía alrededor de 1600 botellas por hora con una cantidad similar de cavidades, por lo que el aumento a 2400 botellas por hora ha mejorado significativamente nuestra utilización de la capacidad. El consumo de energía también es menor a pesar de la mayor producción, lo que ha complacido especialmente a nuestro equipo de operaciones. La compatibilidad de la máquina con múltiples grados de PET ha sido muy útil, ya que nuestros clientes utilizan diferentes especificaciones de resina. Basándonos en esta experiencia, ya estamos planificando la adquisición de una segunda unidad para el próximo ejercicio fiscal.
Información adicional
| Editado por | Yjx |
|---|
Productos relacionados
-
EPA.ES-4C76 Máquina de moldeo por soplado totalmente automática para botellas de pesticidas y productos químicos
-

EPA.ES-4C76 Máquina de moldeo por soplado totalmente automática para botellas de productos químicos de uso diario y cosméticos.
-
EPA.ES-2C260 Máquina de moldeo por soplado totalmente automática para botellas de productos químicos de uso diario y cosméticos.
-
EPA.ES-1C130 Máquina de moldeo por soplado totalmente automática para frascos y latas de boca ancha para alimentos.


