
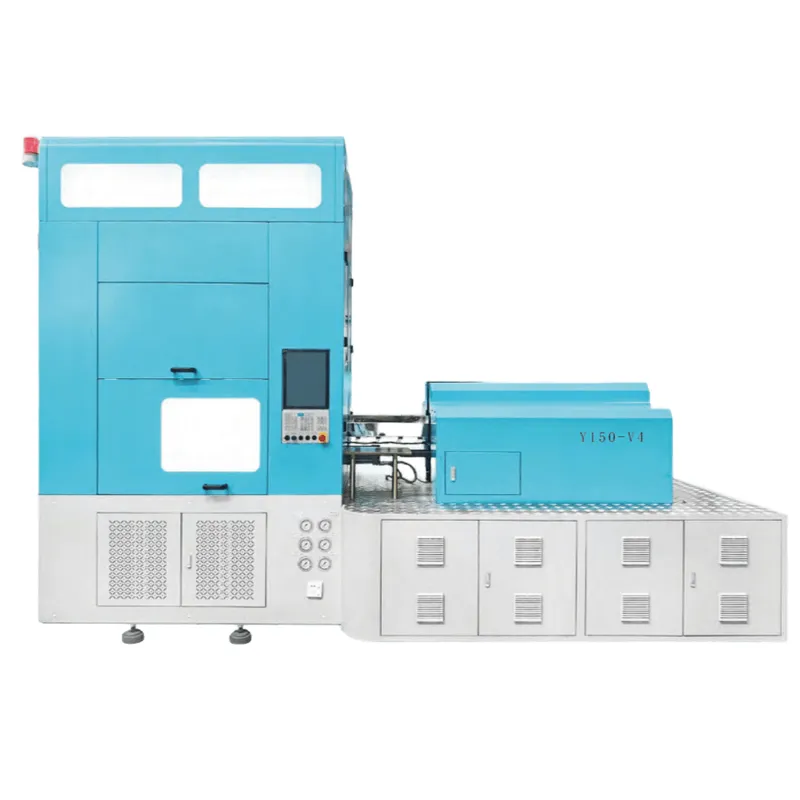
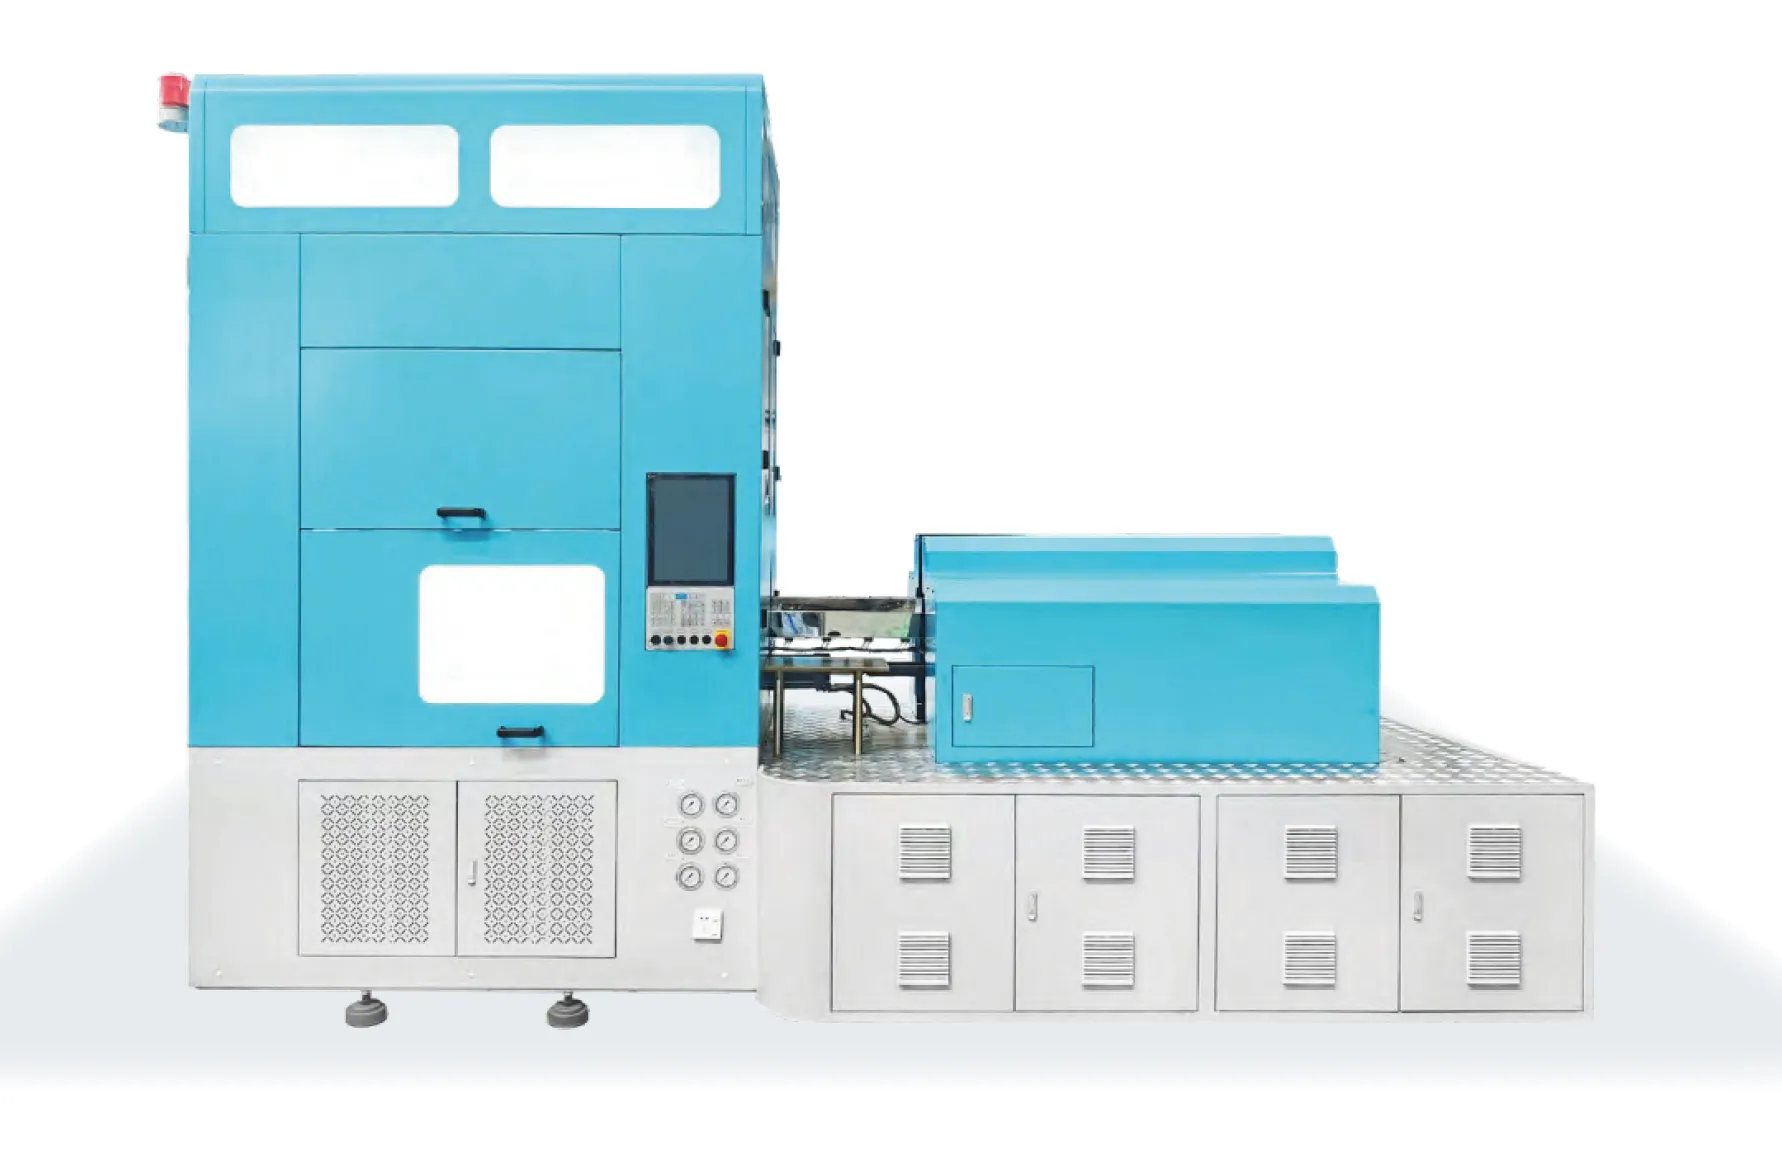
Máquina de moldagem por injeção e sopro Y150-V4-2 - Substituta da ASB-12M japonesa.
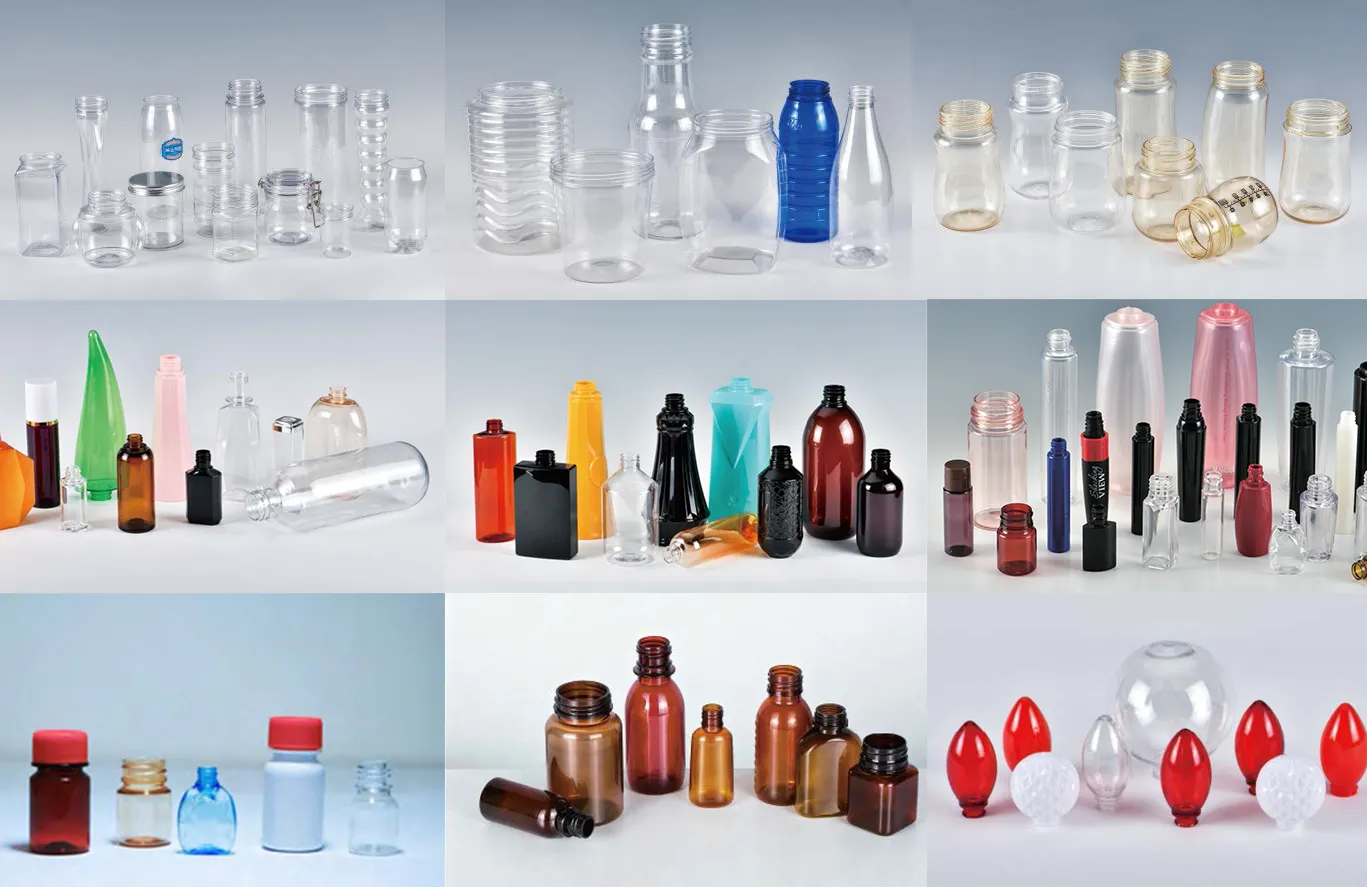
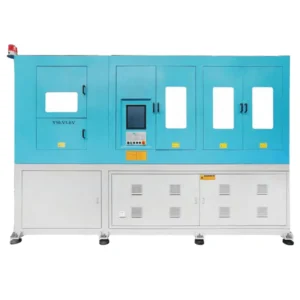
A Y150-V4-2 é uma máquina de moldagem por injeção e sopro de alto desempenho, em um único estágio, projetada como substituta direta do modelo japonês ASB-12M. Desenvolvida e fabricada pela Mexico Ever-Power, esta máquina de moldagem por injeção e sopro em estágio único oferece excepcional diversidade de produtos, produzindo frascos farmacêuticos, frascos cosméticos, mamadeiras, garrafas de água, recipientes de boca larga e frascos com formatos especiais complexos, em uma ampla faixa de volumes, de 20 ml a 2.500 ml.
The Y150-V4-2 is a high-performance one-step injection stretch blow molding machine engineered as a direct replacement for the Japanese ASB-12M model. Designed and manufactured by Mexico Ever-Power, this single stage injection stretch blow molding machine delivers exceptional product diversity, producing pharmaceutical bottles, cosmetic bottles, baby bottles, water glass bottles, wide-mouth containers, and complex special-shaped bottles across a broad volume range from 20 ml to 2,500 ml. Every bottle exits the machine without parting-line marks, satisfying the highest appearance standards demanded by premium brand owners in pharmaceutical, personal care, food, and beverage sectors. The 4-station rotary architecture completes injection, temperature conditioning, stretch-blow, and take-out in one uninterrupted cycle, eliminating reheating energy and intermediate handling steps that add cost and contamination risk.
As a leading injection stretch blow molding machine manufacturer, Mexico Ever-Power built the Y150-V4-2 on a standardized platform using exclusively imported components: Inovance or WEICHI servo motors, a Japan Yaskawa turntable drive, American Parker high-pressure valves, Airtak cylinders, Italian hydraulic tubing, NSK lead screws, and a Taiwan YUKEN hydraulic control valve. This PET injection stretch blow molding machine meets GMP pharmaceutical packaging production standards through a fully contactless production process and offers full servo upgrade options for oil-free operation. Whether you need a customized injection stretch blow molding machine for a proprietary bottle shape or a proven drop-in upgrade for an existing ASB-12M mold set, the Y150-V4-2 delivers the throughput, precision, and reliability your operation demands.
Tabela de comparação de modelos de produtos
1. Substituto para o modelo ASB japonês
| Modelo de máquina Y/YS | Configuração / Observações | Modelo japonês compatível |
| Y150-V4-2 | Configuração padrão | ASB-12M |
| YS150-V4-EV | Servo completo | ASB-12M |
| Y250-V4 | Configuração padrão | ASB-70DPH |
| Y250-V4-B | Série B | ASB-70DPW |
| Y650-V4 | Modelo de grande capacidade | ASB-650 |
2. Substituto para o modelo japonês AOKI
| Modelo de máquina Y/YS | Configuração / Observações | Modelo japonês compatível |
| Y150-V4-B | Série B | SBIII-100L-20 |
| Y150-V3-B | Modelo de 3 estações | SBIII-100L-20 |
| Y200-V4-B | Série B | SBIII-250LL-50S |
| Y200-V3 | Modelo de 3 estações | SBIII-250LL-50S |
| YS350-V4-EV | Servo completo | AL-350LL-40 |
| Modelo padrão | Modelo Servo | Modelo totalmente elétrico |
 |
 |
 |
Nossas vantagens
1. A qualidade é superior. As garrafas de plástico produzidas por máquinas de moldagem por sopro japonesas apresentam uma linha de junção. Há uma saliência de plástico no meio dos dois moldes, em ambos os lados, o que resulta em uma marca. No entanto, nossos moldes possuem altíssima precisão, e a marca é completamente invisível.
2. Nossa produção é rápida, com uma grande quantidade de soluções de rosca e alta velocidade. Enquanto o Japão consegue produzir quatro garrafas plásticas por vez, nós conseguimos produzir seis.
3. Economize energia. Nossas máquinas consomem de 15% a 25% menos energia do que as do Japão, da Europa e dos Estados Unidos.
4. Uma ampla gama de tecnologias de controle elétrico tem sido adotada para substituir componentes hidráulicos e pneumáticos. Por exemplo, os componentes pneumáticos usados no mecanismo de corte inferior no Japão são substituídos por servomotores, e a velocidade dos servomotores é duplicada. Na indústria farmacêutica e em outros setores, servomotores podem ser usados sem a necessidade de sistemas hidráulicos, garantindo a conformidade com as normas GMP e a operação em um ambiente livre de óleo e poluição.
Especificações do produto
| Item | Unidade | Especificações | |||||||
| Nome | Moldagem por sopro e estiramento por injeção em uma única etapa Máquina (4 estações) |
||||||||
| Modelo | Y150-V4-2 (Compatible with Japanese ASB-12M model) | ||||||||
| Fabricante | México Ever-Power | ||||||||
| Material | PET/PETG | ||||||||
| Diâmetro do parafuso | MM | 40 | 50 | 55 | 60 | ||||
| Volume teórico de injeção | CM³ | 188 | 310 | 380 | 480 | ||||
| Velocidade de rotação do parafuso (RPM) | r/min | 270 | 180 | 150 | 150~220 | ||||
| Força de fechamento da injeção | KN | 150 | |||||||
| Força de fixação por sopro | KN | 200 | |||||||
| Potência do motor | KW | 43.2 | |||||||
| Potência de aquecimento | KW | 10 | |||||||
| Pressão do ar soprando | Mpa | 2.0-3.5 | |||||||
| Pressão da água de refrigeração | Mpa | 0.4-0.6 | |||||||
| Pressão da água do resfriador de óleo da máquina | Mpa | 0.3-0.4 | |||||||
| Temperatura da água do resfriador de óleo da máquina | ℃ | 20-25 | |||||||
| Tensão | V | 370-400 | |||||||
| Tamanho (C*L*A) | MM | 4200x1400x2900 | |||||||
| Peso | T | 6 | |||||||
| Dimensões do produto | |||||||||
| Quantidade de produtos | PCS | 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 |
| Diâmetro da garrafa | MM | 118 | 80 | 66 | 56 | 54 | 45 | 28 | 26 |
| Altura da garrafa | MM | 210 | 150 | 100 | |||||
| Diâmetro do pescoço | MM | 83 | 62 | 48 | 38 | 32 | 25 | 17 | 15 |
| Volume máximo da garrafa | ML | 2500 | 1500 | 900 | 400 | 250 | 100 | 30 | 20 |
| Peso máximo da garrafa | G | 130 | 65 | 43 | 32 | 26 | 22 | 18 | 16 |
Parâmetro da máquina
| Modelo compatível: | Compatível com o modelo japonês ASB-12M |
| Diâmetro do parafuso: | 50mm (opcional) |
| Capacidade teórica de injeção: | 310g |
| Força de fechamento da injeção: | 150 kN |
| Curso superior do molde: | 250 mm |
| Curso inferior do molde: | 205 mm |
| TEMP. Regulação do fluxo sanguíneo central: | 250 mm |
| TEMP. regulando o curso do cano: | 230 mm |
| Golpe de retirada: | 170 mm |
| Força de fixação por sopro: | 200 kN (lado único) |
| Golpe central de sopro: | 250 mm |
| Método de moldagem por sopro: | 75+75mm |
| Volume do tanque de óleo: | 300L |
| Dimensões (C×L×A): | 4,2 x 1,4 x 2,9 m |
| Peso: | 6T |
Norma Técnica
| Sistema de controle servo: | Utilizando 3 conjuntos de sistemas de servobombas. |
| Potência do servomotor: | Potência do servo motor Inovance / WEICHI: 43,2KW. |
| Sistema de controle computadorizado: | Utilizando o PLC Inovance/MiRLE. |
| Acionamento do prato giratório: | O toca-discos está equipado com um servomotor Yaskawa do Japão ou um servomotor WEICHI com um redutor TSUNTIEN de Taiwan. |
| Válvula de Alta Pressão: | Utilizando a válvula de alta pressão americana Parker. |
| Cilindro de ar: | Utilizando o cilindro de ar Aitak. |
| Controle de temperatura: | Utilizando uma caixa de controle integrada para controlar a temperatura, que é altamente precisa, estável e fácil de operar; alternativamente, você pode escolher o sistema de controle de temperatura embutido no sistema. |
| Válvula de controle de pressão hidráulica: | Utilizando uma válvula de controle de pressão hidráulica da YUKEN, de Taiwan, China; |
| Tubo de óleo: | O tubo de óleo é feito de material importado da Itália. |
| Parafuso: | O parafuso é aquecido por um anel de aquecimento nano-infravermelho distante com baixo consumo de energia (10 kW). |
| Estrutura de Moldagem por Sopro: | A estrutura de moldagem por sopro adota um sistema de fechamento do molde com cilindro hidráulico ou servomotor duplo com função de compensação de alta pressão. |
| Unidade de Injeção: | A unidade de injeção é controlada por um único cilindro. O motor de fusão pode ser controlado hidraulicamente ou por um servomotor. |
| Potência total da máquina: | Potência total da máquina: 53,2 kW. |
Features of Y150-V4-2 Injection Stretch Blow Molding Machine
1. Zero Parting-Line Marks
Japanese ASB-series machines produce bottles with a visible parting-line protrusion at the mold seam. The Y150-V4-2 uses ultra-precision mold engineering that eliminates this defect entirely, delivering a seamless, glass-like surface finish. For luxury cosmetic bottles and high-end pharmaceutical containers where appearance directly affects brand equity, this difference is decisive and eliminates costly secondary polishing operations.
2. Higher Output Per Cycle
Where a standard Japanese ASB-12M produces 4 bottles per cycle, the Y150-V4-2 produces up to 6 bottles per cycle with a high-speed screw rotational option. The large-volume screw solution combined with optimized cycle timing boosts throughput significantly without increasing floor space. This one step Máquina ISBM architecture removes all intermediate transfer steps, meaning every second of machine time translates directly into saleable product.
3. 15~25% Lower Energy Consumption
The Y150-V4-2 consumes 15% to 25% less energy than comparable Japanese, European, and American machines. This is achieved through three servo pump systems that provide power only on demand, nano far-infrared heating rings that transfer heat more efficiently than conventional elements, and a one-step process that eliminates the reheating stage entirely. Over a typical production year, the energy saving translates into significant reductions in operational cost, directly improving your plant's profitability.
4. GMP-Compliant Contactless Production
The fully enclosed 4-station rotary process operates without human contact from preform to finished bottle. Pneumatic bottom-cutting components used in Japanese machines are replaced by servo motors on the Y150-V4-2, doubling the speed and eliminating oil contamination risk. Pharmaceutical and nutraceutical customers can optionally specify a fully servo, oil-free configuration that meets stringent GMP pharmaceutical packaging production standards, qualifying finished bottles for direct fill applications without secondary cleaning.
5. ASB-12M Mold Compatibility
The Y150-V4-2 is fully compatible with existing Japanese ASB-12M molds, making it the most practical upgrade path for facilities already running ASB-12M equipment. Your existing tooling investment is preserved, transition risk is minimised, and changeover time is minimal. This replacement of ASB ISBM machine approach enables manufacturers to achieve a significant productivity and quality improvement without the full capital and validation cost of replacing both machine and moulds simultaneously.
6. Standardised Imported-Component Design
Every critical component is sourced from globally recognised brands: Parker valves, Yaskawa turntable drives, Airtak cylinders, NSK lead screws, and Italian hydraulic tubing. This standardised architecture means spare parts are universally available, service engineers worldwide can support the machine, and mean-time-to-repair is minimised. For global manufacturers operating multiple production sites, the consistent component specification across Ever-Power's injection stretch blow molding machine range reduces spare-parts inventory and simplifies maintenance training.
Princípio de funcionamento
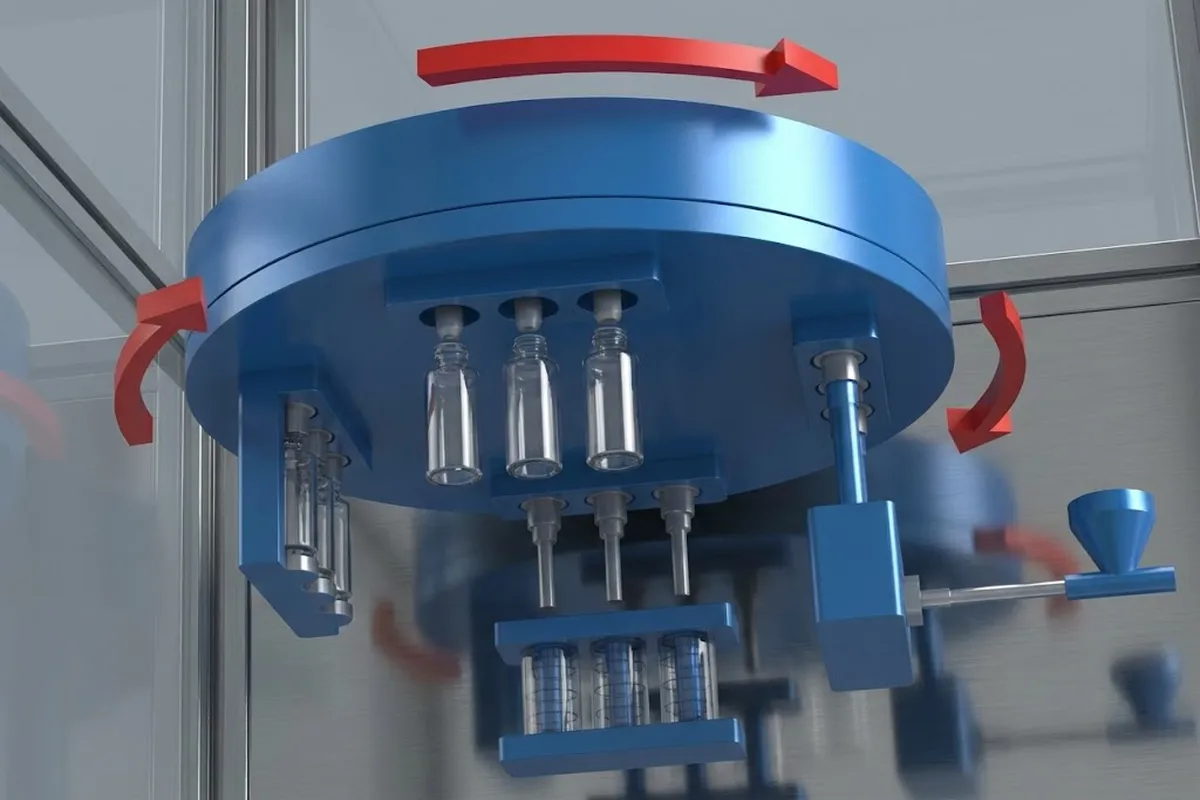
1. Injection Molding
The process begins by heating PET or PETG resin to a molten state using the nano far-infrared heated 50 mm screw. The molten resin is injected at 150 KN clamping force into a precision mold cavity to form a preform. The preform is partially cooled to stabilise its shape while retaining sufficient heat to allow stretching in the next station. Critically, the preform neck finish is formed to its final dimensions at this stage, ensuring reliable sealing and dimensional accuracy throughout the container lifecycle.
2. Preform Conditioning and Transfer
The Yaskawa-servo-driven turntable indexes the freshly moulded preform from the injection station to the temperature conditioning zone with a TEMP. regulating core stroke of 250 mm and a barrel stroke of 230 mm. Controlled heating areas stabilise the preform internal temperature profile. This consistent thermal conditioning ensures uniform material behaviour during the stretch and blow stages, improving container wall uniformity and reducing the risk of whitening, thinning, or dimensional defects. No reheating oven is required, directly eliminating 40% of the energy consumption of two-step processes.
3. Moldagem por sopro com estiramento
This is the defining stage of the single-stage injection stretch blow molding machine process. The blow core (250 mm stroke) descends while the blow mold closes at 200 KN (single side) with a 75 + 75 mm mold stroke. Biaxial stretching begins as a stretch rod extends the preform lengthwise, followed by compressed air at 2.0 to 3.5 MPa inflating it outward to match the mold cavity precisely. This dual-direction molecular alignment enhances the container strength, clarity, barrier properties, and surface gloss, resulting in bottles that consistently outperform two-step blown alternatives in drop-impact and gas-permeation testing.
4. Cooling and Ejection
Once the bottle has been fully blown to its final shape, the machine cooling water circuit (0.4 to 0.6 MPa, 20 to 25 degrees C oil cooler) rapidly solidifies the container inside the mold. After sufficient cooling, the mold opens and the take-out mechanism (170 mm stroke) automatically ejects the finished bottle at the fourth station. The completed container is ready for immediate downstream filling or packaging with no secondary operations required. The integrated cycle then immediately repeats, maintaining continuous high-speed production with no operator intervention between shots.
Applications of ISBM Machines
Frascos farmacêuticos
The Y150-V4-2 produces oral liquid bottles, tablet containers, and dropper bottles in PET and PETG from 20 ml to 400 ml with zero human contact. The GMP-compliant, oil-free servo configuration is approved for direct pharmaceutical packaging lines. Dimensional precision at the neck finish ensures leak-free closure engagement and meets international pharmacopoeia container specifications for moisture vapour transmission and chemical inertness.
Frascos de cosméticos
High-end skincare, perfume, and personal care brands demand flawless surfaces and complex geometry. The parting-line-free finish delivered by the Y150-V4-2 removes the need for post-moulding polishing and enables intricate decorative forms, including oval, faceted, and asymmetric shapes, that a two-step machine cannot reproduce reliably. Container capacities from 20 ml to 2,500 ml cover the full cosmetic range from travel-size serums to pump-top moisturisers.
Frascos de produtos químicos
Household and industrial chemical products require robust containers with excellent barrier properties against volatile organic compounds and aggressive solvents. PET containers produced by this injection blow molding machine platform offer superior gas-barrier performance over untreated HDPE, extending product shelf life and reducing material usage through thinner walls. The machine handles screw diameters up to 60 mm to accommodate higher-viscosity material blends used in speciality chemical applications.
Garrafas de comida
From condiment jars and cooking oil bottles to wide-mouth food canisters, the Y150-V4-2 produces food-grade PET containers with crystal clarity that showcases product colour and texture at the point of sale. The contactless process eliminates contamination risk for food-contact surfaces, and biaxial orientation improves carbon dioxide and oxygen barrier performance, extending refrigerated and ambient shelf life without the cost of active barrier coatings.
Mamadeiras
Baby feeding bottles impose the most demanding combination of clarity, impact resistance, thermal stability, and food-contact safety. The Y150-V4-2 processes PETG, which offers glass-like transparency and can withstand repeated sterilisation at elevated temperatures. Production in a clean, oil-free environment and zero parting-line surface quality meet the expectations of premium baby product brands in regulated markets such as the EU, USA, and Japan, where safety documentation and dimensional consistency are non-negotiable.
Pesticide Bottles
Agricultural chemical packaging requires high chemical resistance, robust wall thickness for pressure resistance, and child-resistant neck geometries. The Y150-V4-2 accommodates neck diameters from 15 mm to 83 mm and volumes up to 2,500 ml, covering the full range of pesticide bottle formats from concentrated formulation ampoules to pump-sprayer containers. PET barrier performance and weld-seam integrity are critical for preventing leakage, spillage, and regulatory non-compliance during distribution and storage.
Frascos de sabonete líquido
Body wash, shampoo, and liquid soap bottles benefit from the smooth, lustrous surface finish produced by the Y150-V4-2, which eliminates the parting seam that compromises label adhesion and visual quality. The machine readily handles pump-top, flip-cap, and disc-top neck finishes in a single tool, and supports oval and square cross-section bottles that stand out on retail shelves. Batches can run without interruption for extended periods, supporting the high-volume output required by private-label contract manufacturers.
Cooking Oil Bottles
Edible oil containers demand excellent clarity to showcase product colour, high rigidity to survive distribution stacking, and tight-tolerance neck dimensions for reliable cap sealing under the positive pressure of hot-fill applications. The Y150-V4-2 produces PET cooking oil bottles from 250 ml to 2,500 ml at the required wall thickness, with the biaxial molecular orientation delivering the compressive column strength needed for pallet stacking without deformation, a key requirement for large-format retail club packs and bulk wholesale distribution.
Key Equipment Components
Unidade de Fixação
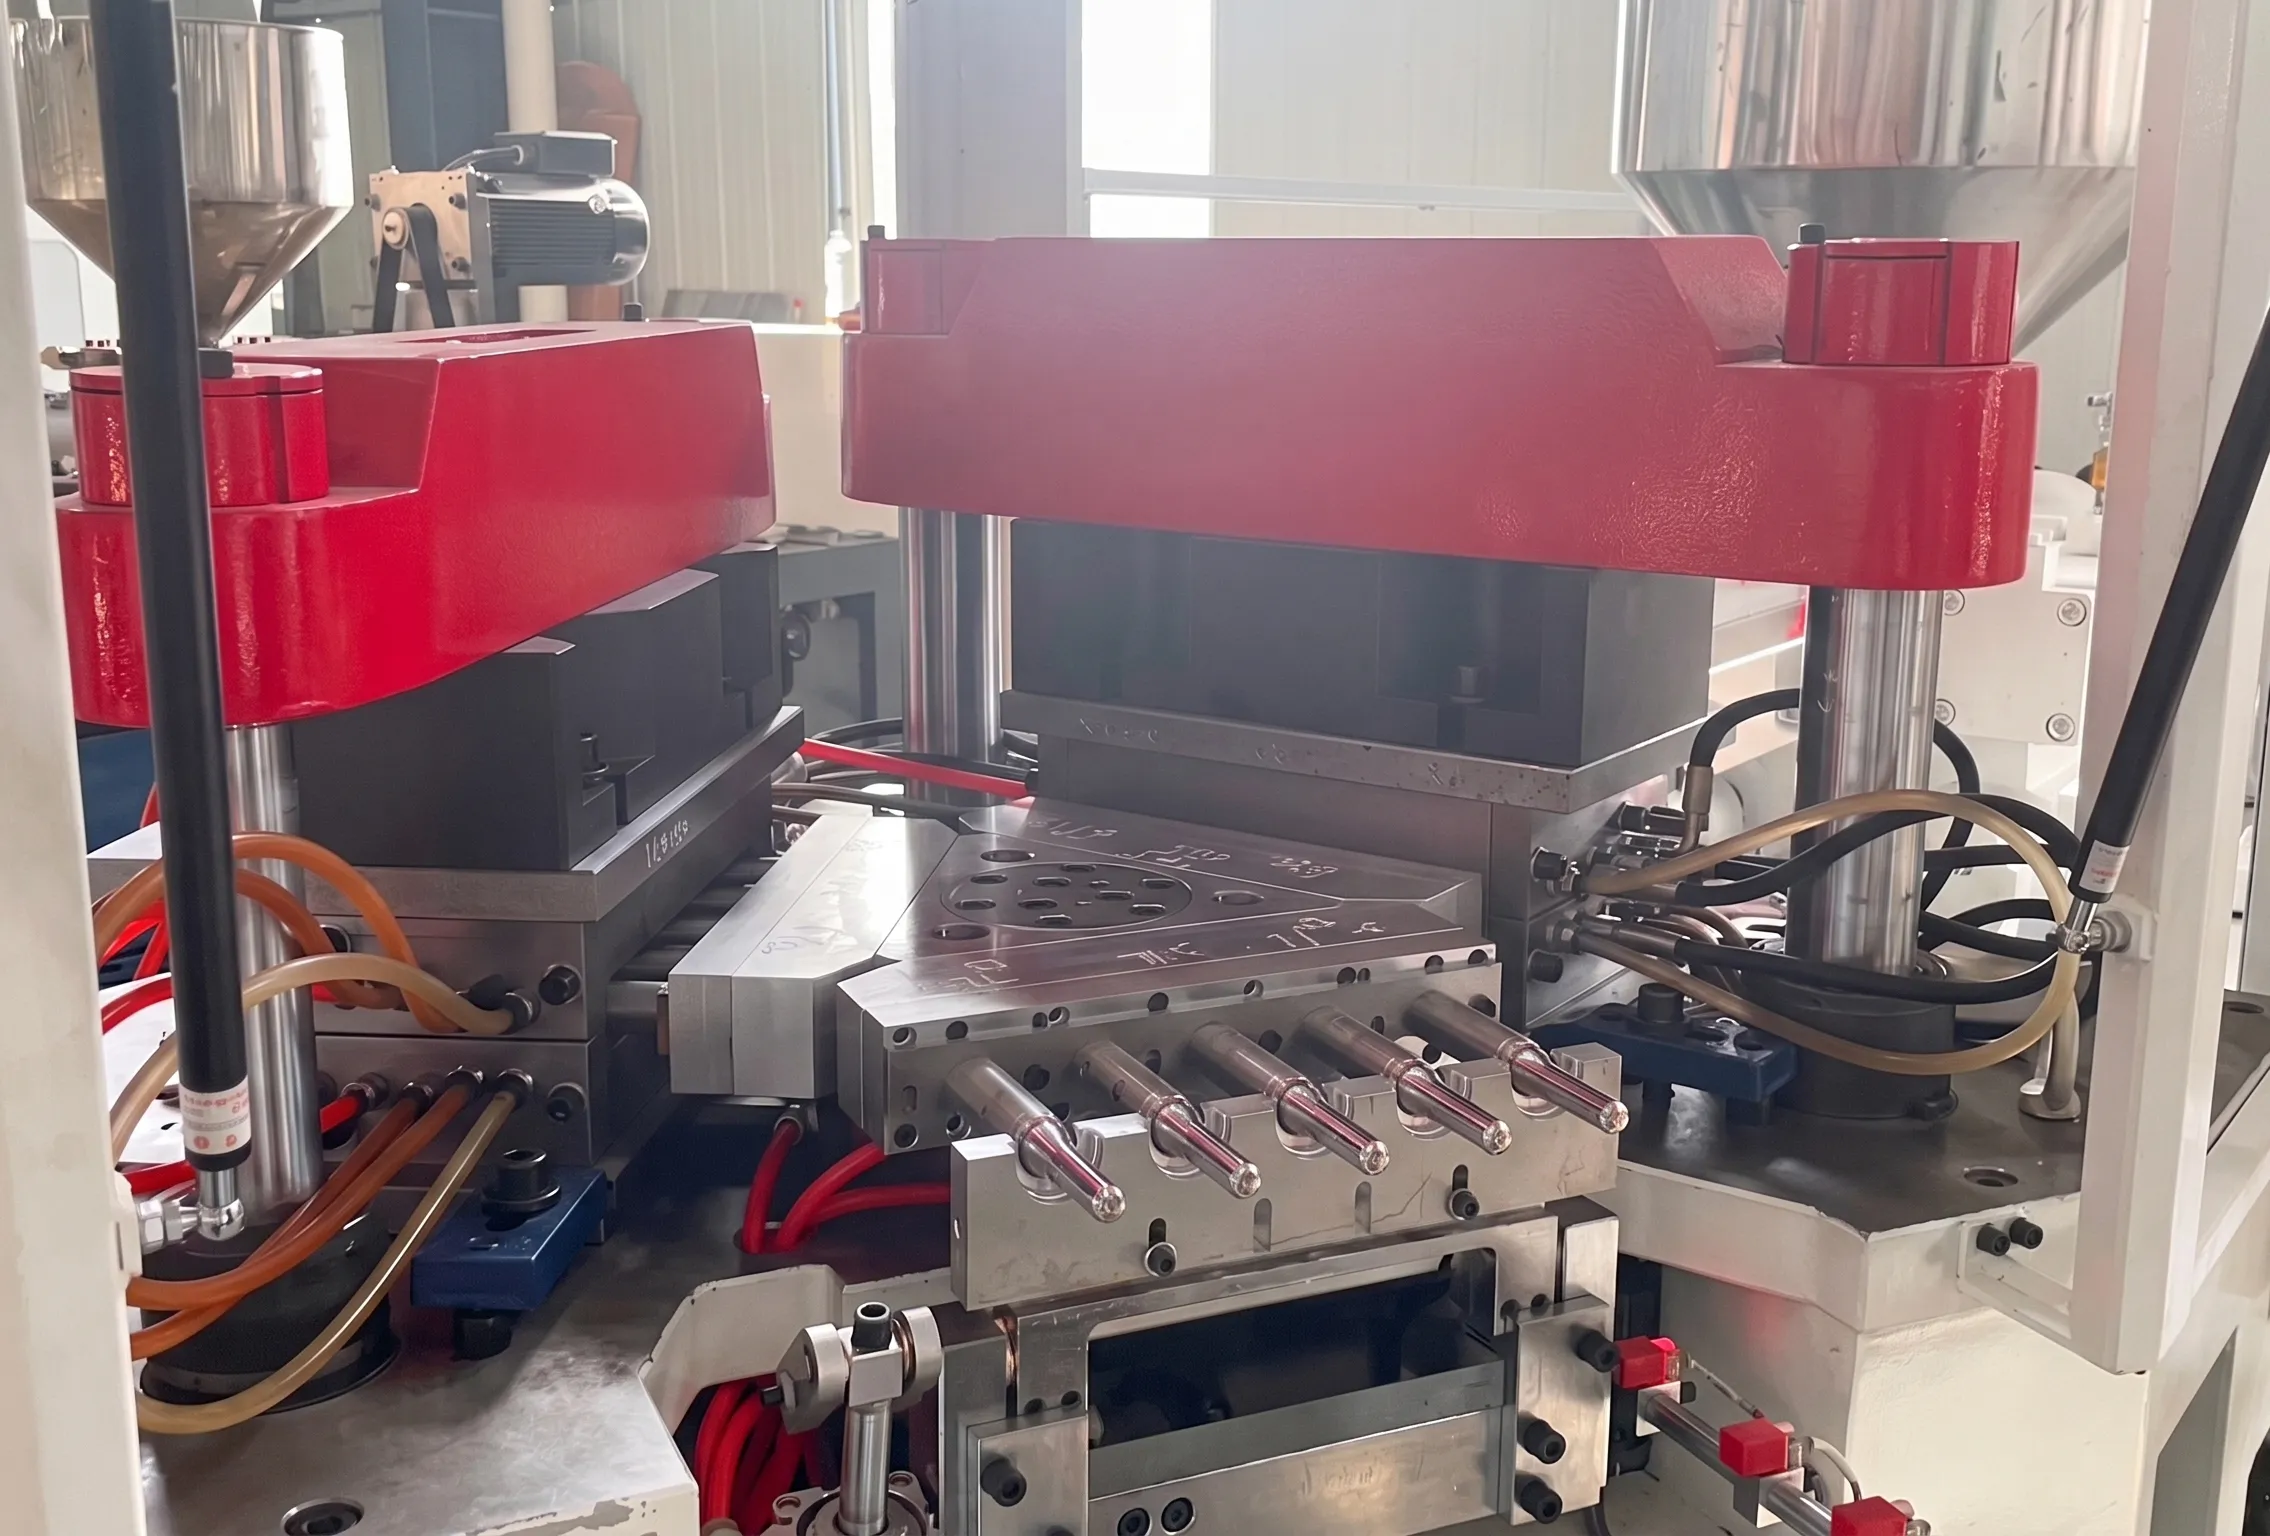
The injection clamping unit delivers 150 KN of force with upper and lower mold strokes of 250 mm and 205 mm respectively. The blow clamping unit provides 200 KN (single side) with a 75 + 75 mm blow mold stroke. High-pressure compensation function ensures consistent cavity pressure distribution regardless of mold wear state, protecting tooling longevity and maintaining bottle wall uniformity across extended production runs on this customized injection stretch blow molding machine platform.
Unidade de Injeção
A single-cylinder injection unit controls the melt delivery with a 50 mm (optional) screw delivering up to 310 g of theoretical injection capacity at rotational speeds from 150 to 270 r/min depending on screw diameter selection. The melt motor may be controlled hydraulically or by servo motor, offering flexibility for standard or fully-electric GMP configurations. The nano far-infrared 10 KW heating ring maintains precise melt temperature with minimal thermal gradient across the barrel length.
Sistema de moldagem
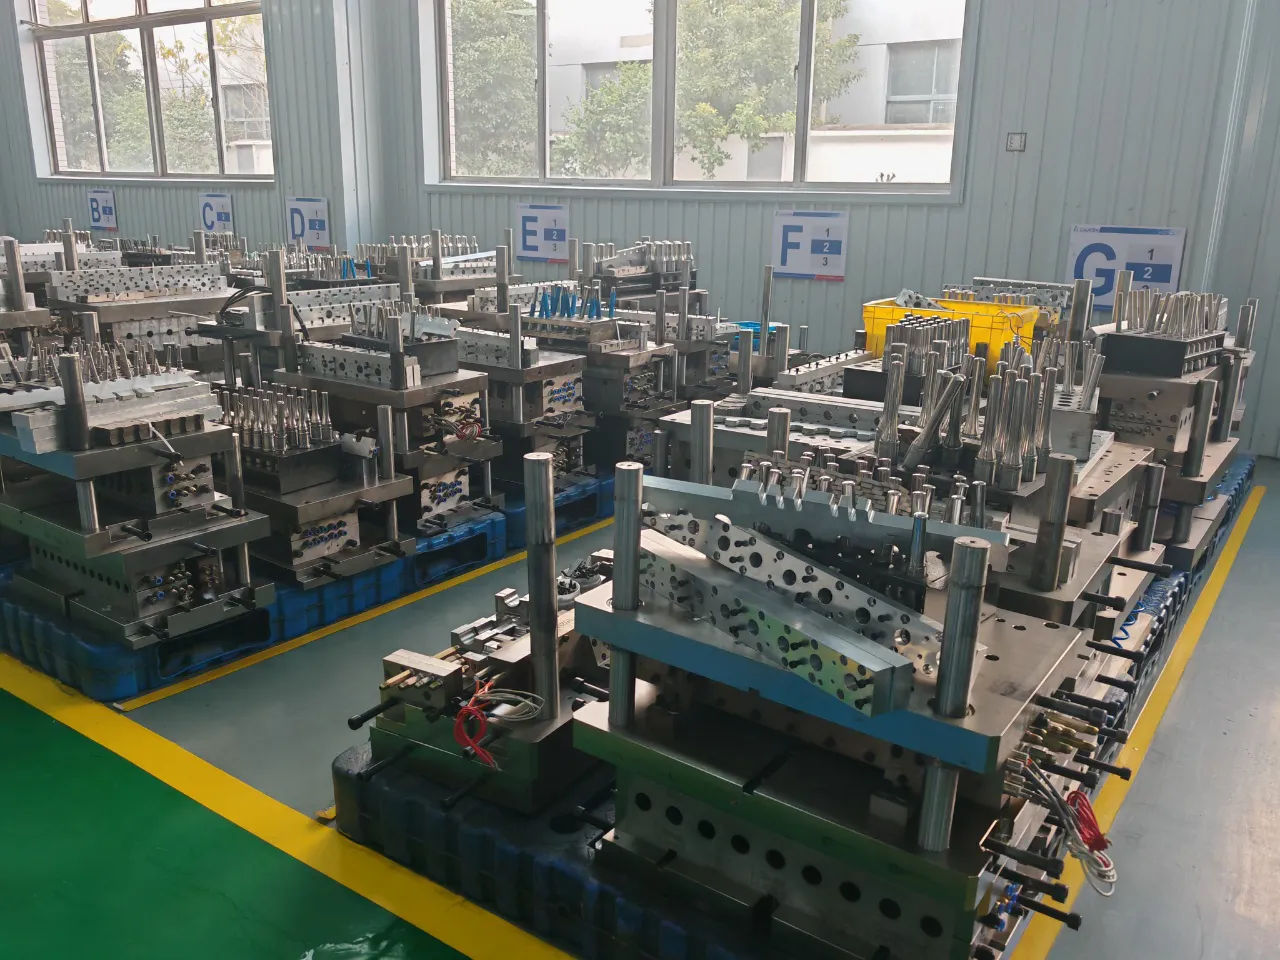
The Y150-V4-2 is fully compatible with Japanese ASB-12M moulds, preserving your existing tooling capital. Ever-Power also offers ISBM mold injection machines supplier services including custom mold design and manufacturing for proprietary bottle shapes from 20 ml to 2,500 ml. Mold cavities are machined to ultra-high precision tolerances that eliminate visible parting-line marks and deliver the glass-smooth surfaces required by pharmaceutical and premium cosmetic customers without post-processing.
Sistema de pino de sopro
The blow core operates on a 250 mm stroke and delivers clean, precisely timed high-pressure air at 2.0 to 3.5 MPa via the American Parker high-pressure valve. The blow pin geometry is matched to each specific neck finish to ensure uniform air distribution inside the preform during biaxial stretching. This precise air delivery is the primary factor governing container wall thickness uniformity, optical clarity, and carbon dioxide barrier performance in the finished PET bottle, all areas where the Y150-V4-2 consistently outperforms competitors.
Sistema de refrigeração
Two independent cooling circuits manage the machine thermal envelope: a mold cooling water system operating at 0.4 to 0.6 MPa for rapid bottle solidification, and a machine oil cooler circuit at 0.3 to 0.4 MPa maintaining hydraulic oil temperature at 20 to 25 degrees C. Rapid in-mold cooling directly determines achievable cycle time: the faster and more uniform the cooling, the shorter the blow station dwell time, and the higher the machine output per hour under sustained production conditions.
Sistema de Ejeção
The take-out mechanism operates on a 170 mm stroke and is synchronised with the Yaskawa-driven turntable indexing sequence to eject finished bottles at station four without interrupting the upstream injection cycle. Automatic ejection eliminates manual unloading labour and the contamination and variability it introduces. The ejection timing and force are software-adjustable from the Inovance PLC touchscreen interface, enabling fast format changeovers between bottle specifications and supporting a wide range of downstream conveyor and inspection system configurations.
Temperature Control System
An integrated control box manages barrel, mold, and conditioning zone temperatures simultaneously with high accuracy and stability. Operators may alternatively select the system built-in temperature control for simplified parameter management. Consistent inter-zone temperature gradients are the primary factor determining preform stretch behaviour uniformity, and the precision of this system is the key reason why the Y150-V4-2 produces bottles with markedly lower wall-thickness variation compared to two-step reheat blow moulding alternatives.
Servo Drive Architecture
Three sets of servo pump systems replace conventional fixed-displacement hydraulic pumps, providing energy only when and where it is required. Inovance / WEICHI servo motors (43.2 KW combined) are governed by the Inovance / MiRLE PLC, which provides closed-loop position, speed, and pressure control on every axis. This architecture is the foundation of the machine energy efficiency advantage and is also the enabler of the full servo, oil-free upgrade path available for pharmaceutical and clean-room production environments in this full electric injection stretch blow molding machine variant.
Injection Blow Molding vs Stretch Blow Molding: Key Differences
What Is Injection Blow Molding?
Injection Blow Molding is a two-stage process that combines the dimensional precision of injection moulding with the hollow-forming capability of blow moulding. Molten plastic is first injected into a mold to form a preform whose neck threads are already in their finished form. The preform is then transferred to a blow mold, where compressed air inflates it into the target bottle shape. Ever-Power advanced IBM machine solutions are designed for small, intricate bottles used in pharmaceuticals, cosmetics, and personal care, delivering exceptional dimensional accuracy and tight tolerances with minimal post-processing. Key attributes: high precision, uniform wall thickness, ideal for small to medium containers, suitable for complex neck designs, minimal flash or waste.
What Is Injection Stretch Blow Molding?
Injection Stretch Blow Molding, as implemented in the Y150-V4-2 injection stretch blow molding machine, adds a mechanical stretching step that orients the polymer molecules biaxially before the blowing air is introduced. This molecular alignment substantially improves the container strength-to-weight ratio, optical clarity, gas barrier performance, and surface gloss compared to unstretched blow moulding. The process is the recognised gold standard for PET bottle production in beverage, food, and personal care markets. Key attributes: excellent strength-to-weight ratio, high clarity especially with PET, efficient for large-scale production, ideal for thin-walled lightweight bottles.
Comparative Overview
| Recurso | Moldagem por Injeção e Sopro (IBM) | Moldagem por Injeção e Estiramento por Sopro (ISBM) |
|---|---|---|
| Etapas do processo | Injection + Blow | Injection + Stretch + Blow |
| Compatibilidade de materiais | HDPE, PP, PVC | PET, PETG, PP |
| Tamanho do recipiente | Pequeno a médio | Small to large (20 ml to 2,500 ml) |
| Espessura da parede | Uniform | Optimised (typically thinner and lighter) |
| Resistência mecânica | Bom | Excellent (biaxial orientation) |
| Optical Clarity | Moderado | High (especially with PET) |
| Aplicações típicas | Pharmaceutical, cosmetics | Beverages, food, personal care, pharma |
| Velocidade de produção | Moderado | Alto |
The decision between IBM and ISBM depends on resin type, container geometry, production volume, and cost targets. Use IBM when you need precise neck finishes and uniform walls in small containers for pharmaceuticals or high-end cosmetics. Choose ISBM when you need lightweight, high-clarity, high-strength bottles in volume, such as for water, juice, condiments, or personal care products. Ever-Power provides both injection blow molding machine and injection stretch blow molding machine manufacturers solutions and can advise on the optimal process for your specific container programme.
 |
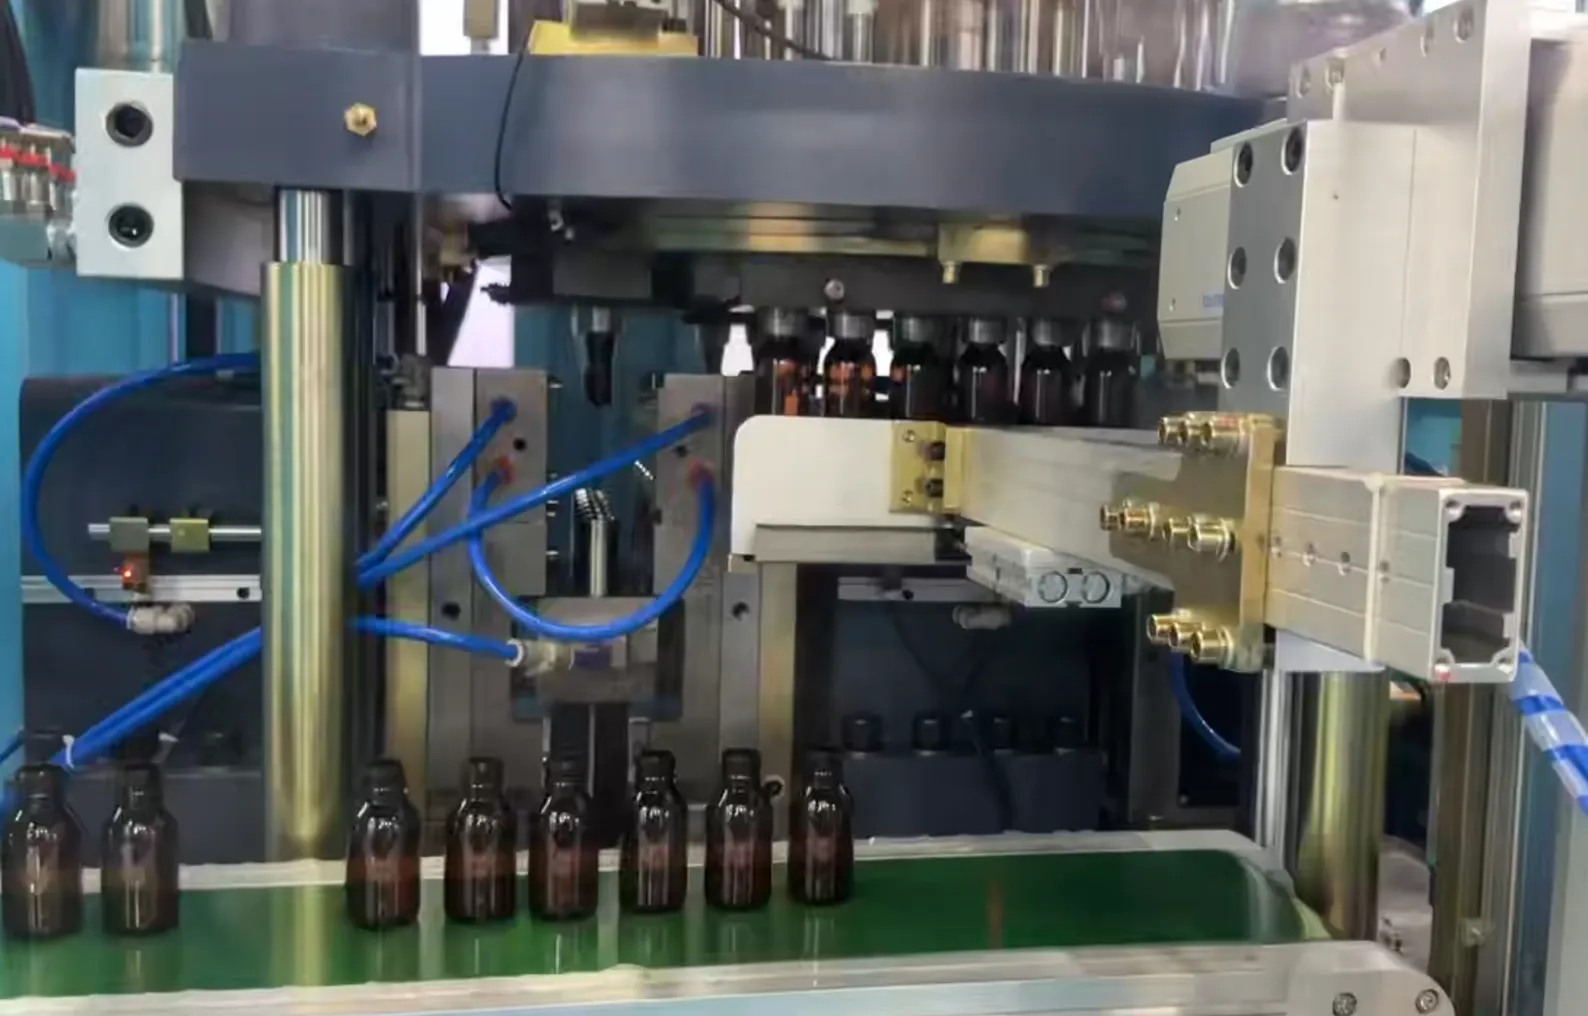 |
| Moldagem por Injeção e Sopro | Moldagem por sopro e estiramento por injeção |
|---|
Materiais Compatíveis
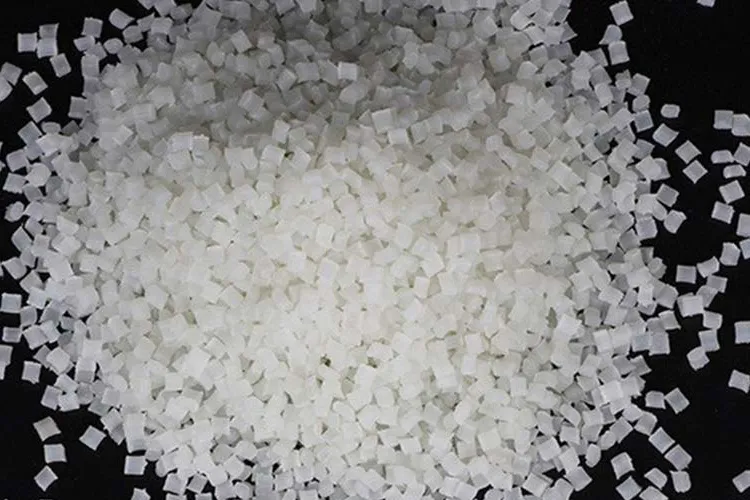
PET (Polietileno Tereftalato)
PET is the primary material for the Y150-V4-2 and the most widely used resin in injection stretch blow molding globally. It is strong, lightweight, and optically clear, making it the default choice for pharmaceutical, beverage, food, and cosmetic bottles. PET also has excellent recyclability credentials, supporting sustainability commitments for brands targeting circular economy standards.
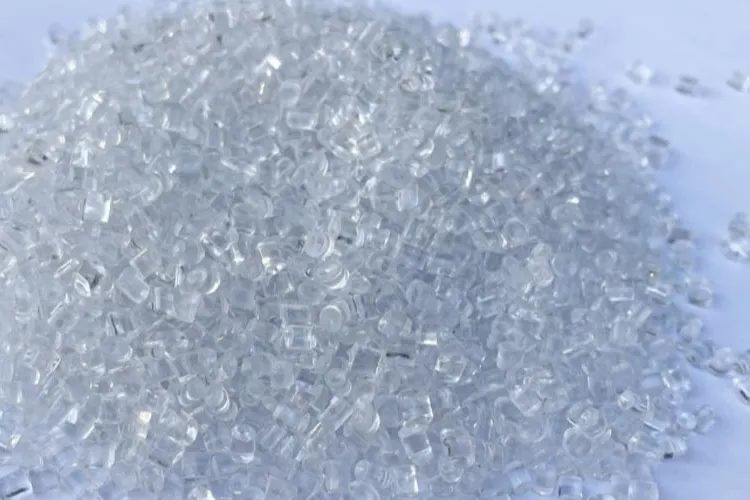
PETG (Polietileno Tereftalato Glicol)
PETG offers the optical clarity of PET with improved impact resistance and the ability to withstand repeated autoclave sterilisation cycles at elevated temperatures. It is the preferred material for baby bottles, medical device packaging, and laboratory containers where both chemical resistance and visual clarity are mandatory. PETG does not crystallise on stretching, enabling greater design freedom in container geometry.
PP (Polipropileno)
PP is a versatile engineering resin suited to both hot-fill and cold-fill applications. Its high melting point makes it the preferred choice for containers that must survive filling temperatures above 85 degrees C, such as pasteurised juice, hot-pack sauce, and sterilised pharmaceutical liquids. PP containers processed on a single stage injection stretch blow molding machine offer good chemical resistance and a lower density than PET, reducing per-container material cost.
PEAD (Polietileno de Alta Densidade)
HDPE is a robust and durable resin widely used in blow moulding for applications requiring moisture, chemical, and UV radiation resistance, making it ideal for outdoor, agricultural, and industrial chemical containers. Its high environmental stress crack resistance suits squeeze-tube and dispensing bottle formats. HDPE is also one of the most widely recycled plastics globally, with established collection and reprocessing infrastructure in most major markets.
PS (Polystyrene)
PS is a rigid, clear resin commonly selected for packaging applications where optical clarity is the primary requirement and impact demands are moderate, such as clear sample cups, cosmetic jars, and electronics protective packaging. Its relatively low cost and ease of processing make it an economical choice for high-volume commodity packaging where premium barrier or impact performance is not required. Specialist grades including high-impact PS expand the application range for durable container formats.
PC (Policarbonato)
PC is an engineering thermoplastic renowned for its exceptional impact resistance and optical clarity, making it the material of choice for sports water bottles, reusable containers, and safety equipment housings. Its very high heat deflection temperature allows sterilisation by boiling or steam. While BPA-free grades have largely replaced traditional PC in food-contact applications, PC remains the standard material for industrial sight glasses, instrument covers, and high-impact specialty containers in the pharmaceutical and laboratory instrument sectors.
 |
 |
 |
 |
 |
 |
How to Choose the Right ISBM Machine
1. Production Volume
Define your required daily or annual output in bottles before evaluating any machine. The Y150-V4-2 4-station platform with up to 6 cavities per cycle is optimised for medium-to-high volume production of specialist containers. If your programme demands very high volumes of a single bottle type, a multi-cavity or multi-station platform such as the HGYS280-V6 six-station machine may offer better economics. Ever-Power application engineers can model your output requirements and recommend the right platform configuration for your specific production programme.
2. Bottle Size and Shape
Match the machine envelope to your bottle specification before committing to a platform. The Y150-V4-2 handles neck diameters from 15 mm to 83 mm, bottle diameters up to 118 mm, and volumes from 20 ml to 2,500 ml. For larger containers up to 20 litres, the HGY650-V4 platform should be considered. For very small vials below 20 ml or bottles with highly complex geometries, share your CAD drawings with Ever-Power engineers early to confirm mold feasibility and identify any special tooling requirements before placing an order.
3. Material Type
The Y150-V4-2 is optimised for PET and PETG. If your process requires PP, HDPE, or PC, confirm with Ever-Power that the screw geometry, barrel temperature profile, and blow pressure specification are correctly matched to your chosen resin. Material grade matters as much as resin family: intrinsic viscosity in PET, MFI in PP, and molecular weight in PC all affect processing behaviour. Ever-Power application engineers can advise on resin specification and, where required, provide material qualification trials before full production commitment.
4. Automation Level
The Y150-V4-2 standard configuration uses three servo pump systems for high repeatability at lower cost. The YS150-V4-EV full servo variant eliminates hydraulic systems entirely, achieving oil-free operation with 10 servo motor control sets for pharmaceutical GMP environments. Consider your clean-room classification, operator headcount targets, and downstream automation integration requirements when specifying the drive architecture. Ever-Power can also integrate vision inspection, checkweighing, and automated reject systems to complete your line.
5. Energy Efficiency
The Y150-V4-2 consumes 15% to 25% less energy than comparable Japanese, European, and American machines through servo-on-demand hydraulics, nano far-infrared barrel heating, and the elimination of the reheating stage. Request an energy audit comparison from Ever-Power using your current machine type and bottle specification to calculate the specific annual energy saving and ROI timeline for your facility. In markets with high industrial electricity tariffs, energy efficiency alone can justify the investment within two to three years of operation.
6. Maintenance and Support
Ever-Power provides comprehensive pre-sale, in-sale, and after-sale support through a team of experienced injection-blowing machinery engineers. All critical components Parker, Yaskawa, Inovance, YUKEN, and Airtak are globally stocked, ensuring fast availability. Ever-Power offers factory acceptance testing before shipment, on-site installation and commissioning, operator training, and a structured maintenance programme. For international customers, remote diagnostics through the Inovance PLC interface minimises engineer travel time and keeps your machine running productively throughout its operating life.
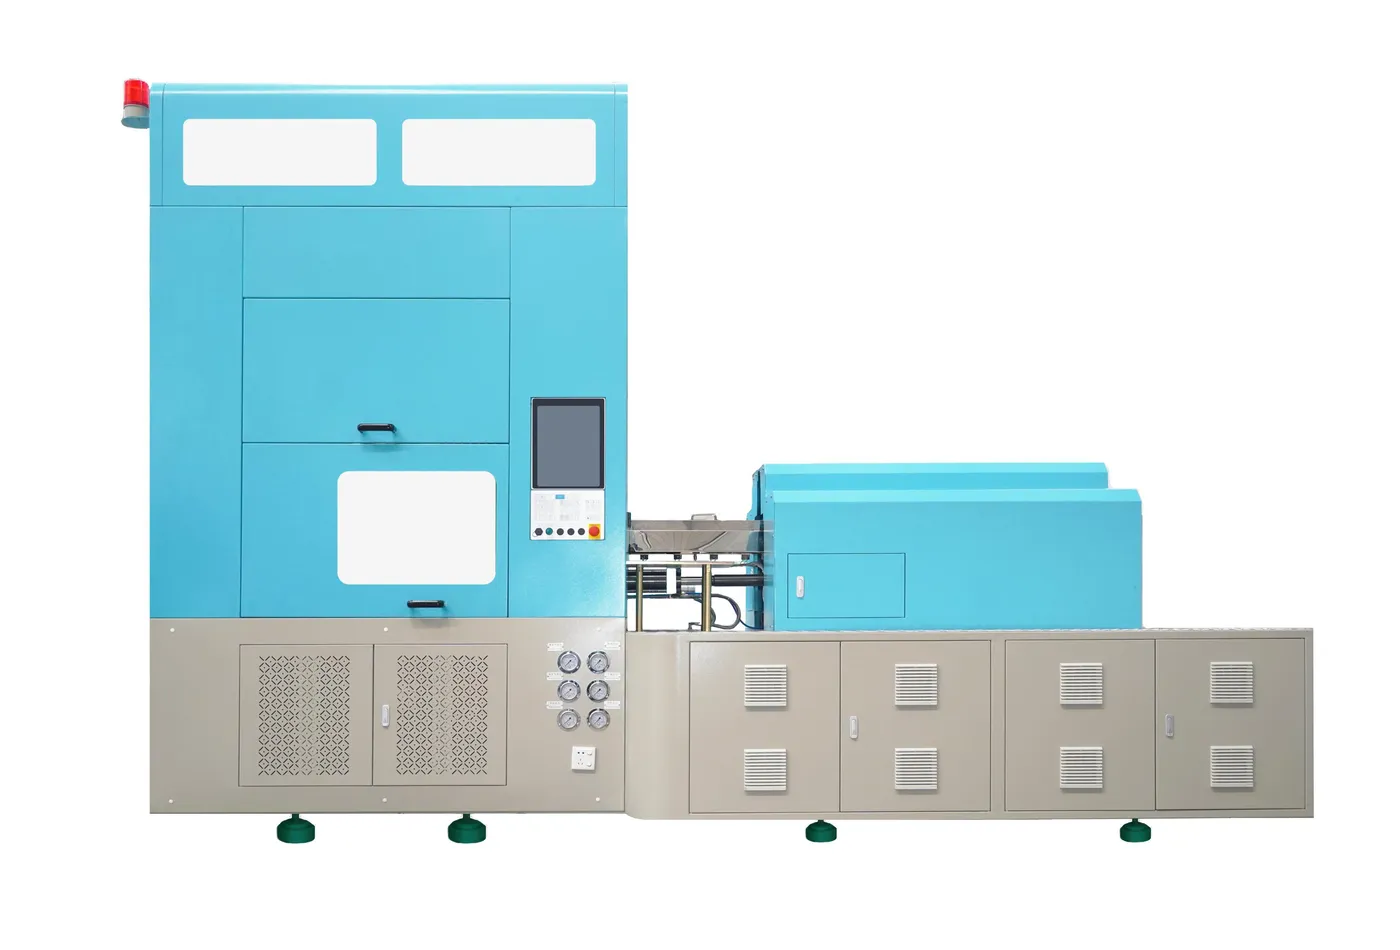
Injection Stretch Blow Molding Machine Maintenance
1. Regular Cleaning
Clean the injection and blowing mold cavities, runners, and vents at the end of each production run to prevent carbon deposit build-up, PET degradation residue, and contamination migration into the next batch. Wipe down all exposed mechanical surfaces, guideways, and the take-out mechanism with a lint-free cloth dampened with the recommended solvent. Compressed air purging of the barrel and screw assembly should follow each material changeover to prevent colour or resin grade cross-contamination.
2. Lubrication Maintenance
Apply the specified lubricating oil to all guide rails, clamping unit tie-bars, turntable bearing races, and the ejection mechanism at the intervals specified in the Ever-Power maintenance schedule, typically every 500 operating hours. NSK lead screws require periodic lubrication with the manufacturer-specified grease rather than oil. Correct lubrication prevents accelerated wear on precision motion components and is the single highest-impact preventive maintenance action for extending machine service life and maintaining dimensional repeatability.
3. Servo and Electric System Check
Verify the operational stability of all three servo pump systems and the Inovance / MiRLE PLC on a monthly basis by reviewing system alarm logs, checking servo drive parameter consistency, and confirming that all motor current draws are within the rated operating range. Inspect encoder connections and communication cables for wear, corrosion, or loose terminations. Servo motor cooling fans should be checked quarterly and cleaned to prevent overheating under sustained high-duty-cycle production conditions.
4. Electrical System Maintenance
Inspect the interior of the main electrical cabinet annually with the machine fully isolated and locked out. Check all terminal connections for signs of heat discolouration or loosening caused by vibration. Verify that cable routing has not created chafe points against sharp enclosure edges. Test the earth bonding continuity across the machine frame to ensure personnel safety. Review and replace any degraded cable insulation, thermal protectors, or contactors identified during the inspection before returning the machine to service to prevent short circuits and production downtime.
5. Mold Maintenance
Inspect all mold cavity surfaces, parting faces, vent slots, and cooling channel connections at regular intervals for wear, erosion, or sealing degradation. Polish cavity surfaces when surface finish begins to transfer to bottle walls, as any scratch or pit in the cavity surface will reproduce on every bottle produced. Check the mold cooling water connections for mineral scale build-up inside channels, which reduces heat transfer efficiency and extends cycle time. Replace worn or damaged mold components immediately to prevent escalating dimensional non-conformance across the bottle population.
6. Machine Parameter Adjustment
Periodically verify and recalibrate all process parameters through the Inovance PLC interface, including injection pressure, screw speed, barrel temperature profile, blow pressure, cycle timing, and cooling water flow rates. Compare current parameter values against the validated baseline established during initial commissioning. Gradual parameter drift caused by component wear or seasonal ambient temperature change is the most common cause of slow-onset quality degradation in continuous production, and systematic parameter auditing is the most effective way to identify and correct it before it reaches customer-visible quality levels.
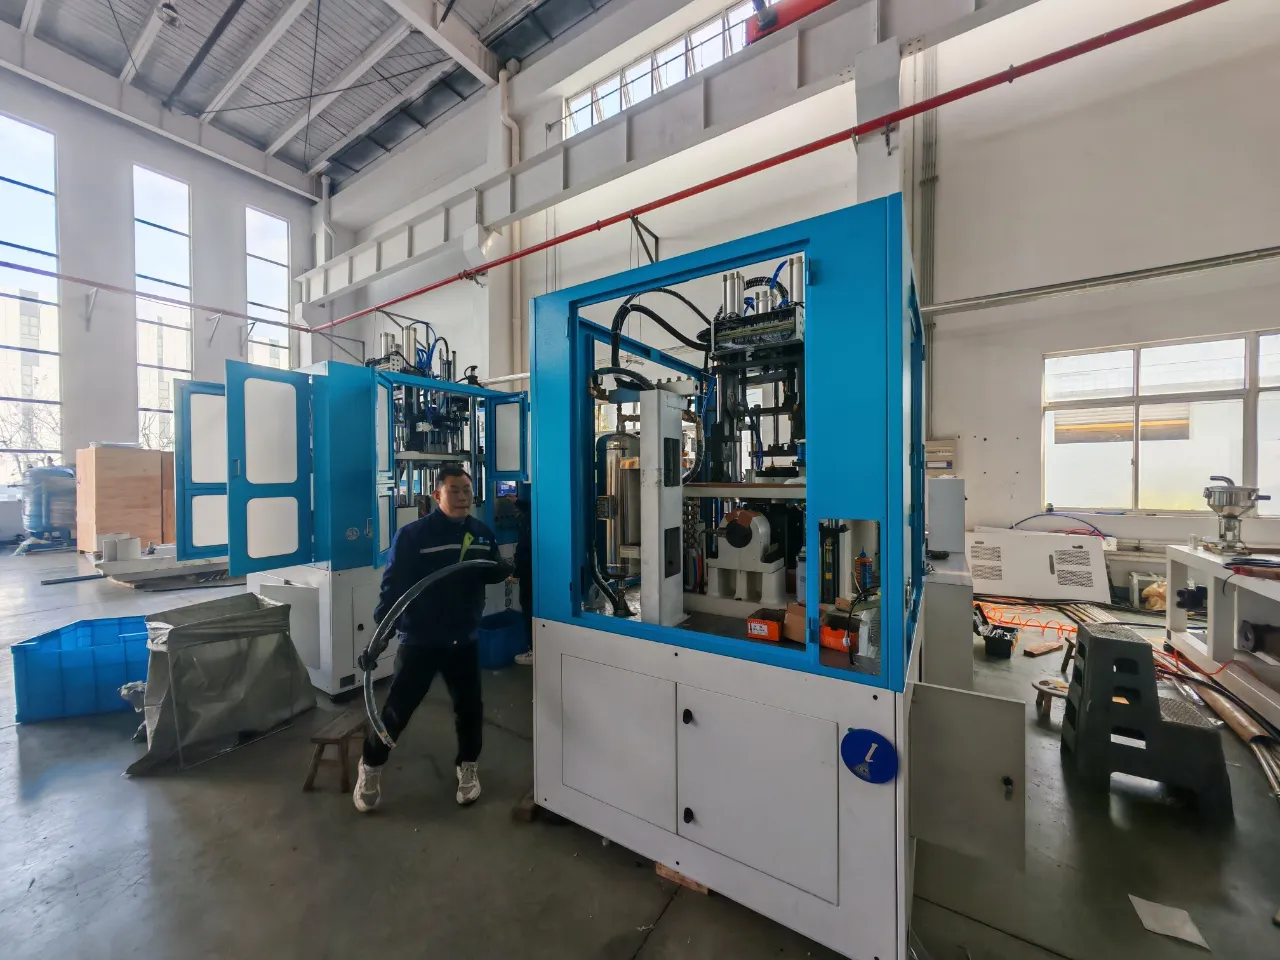
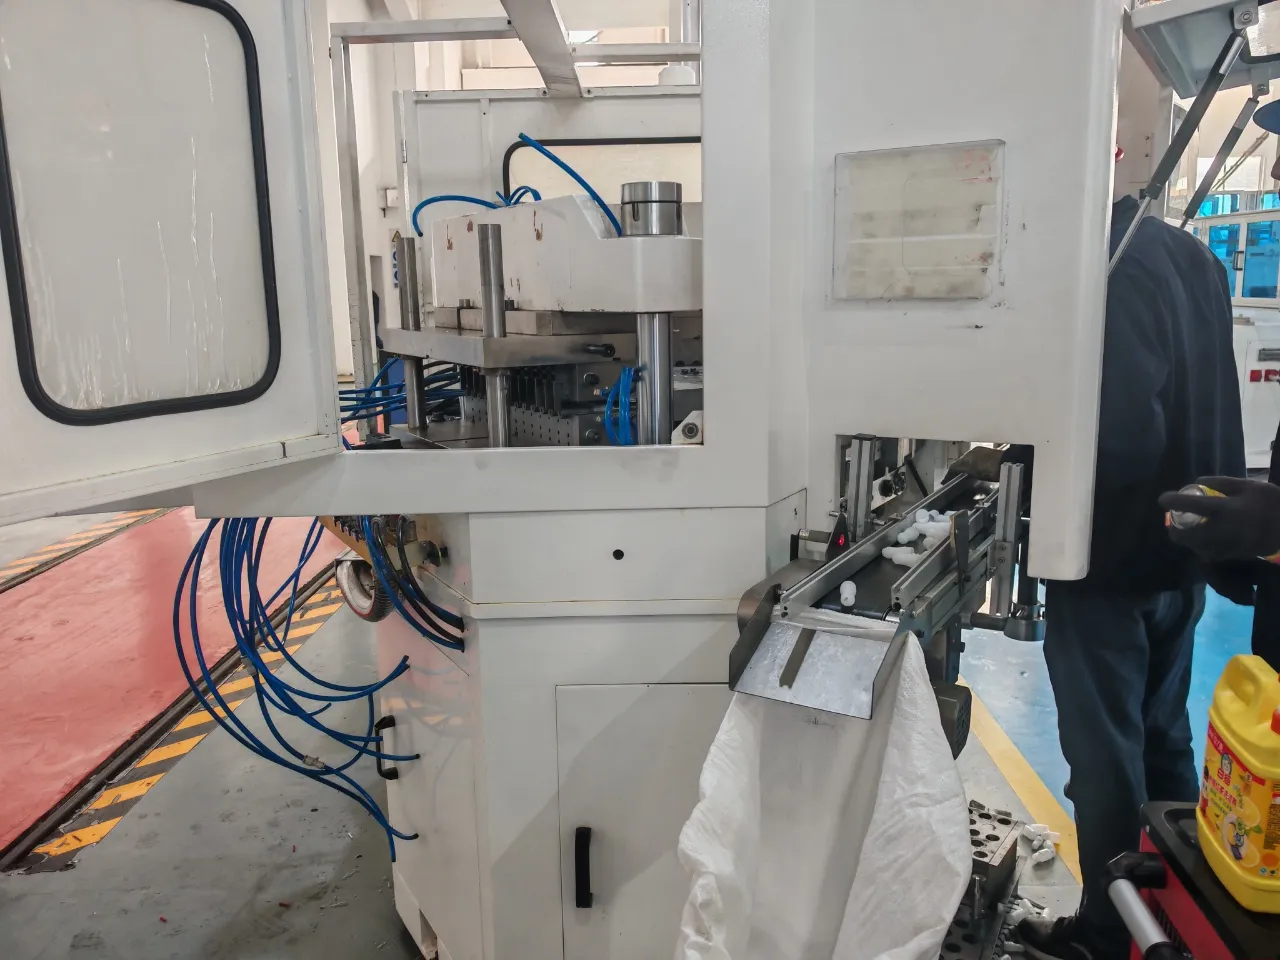
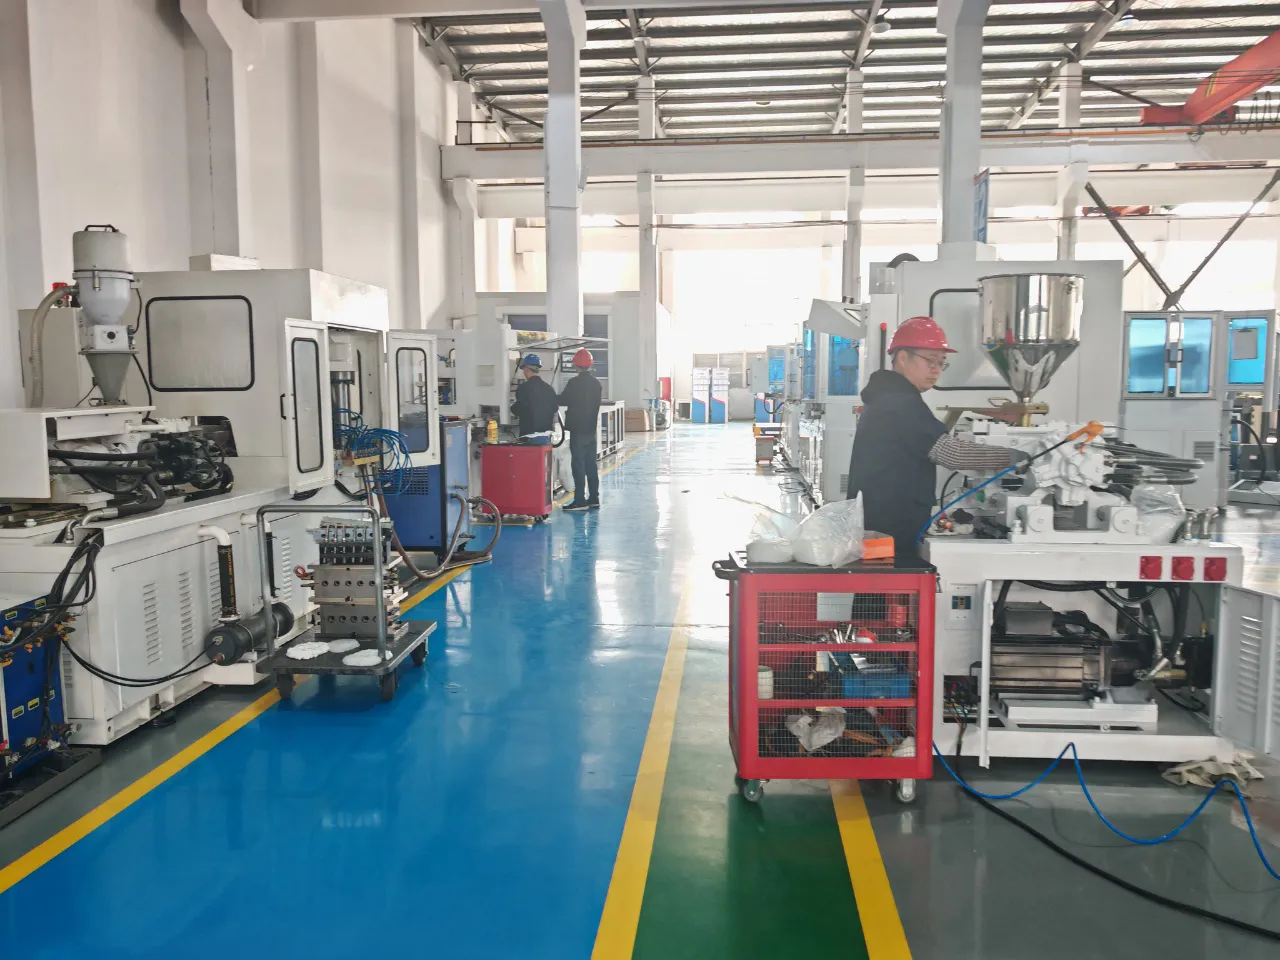
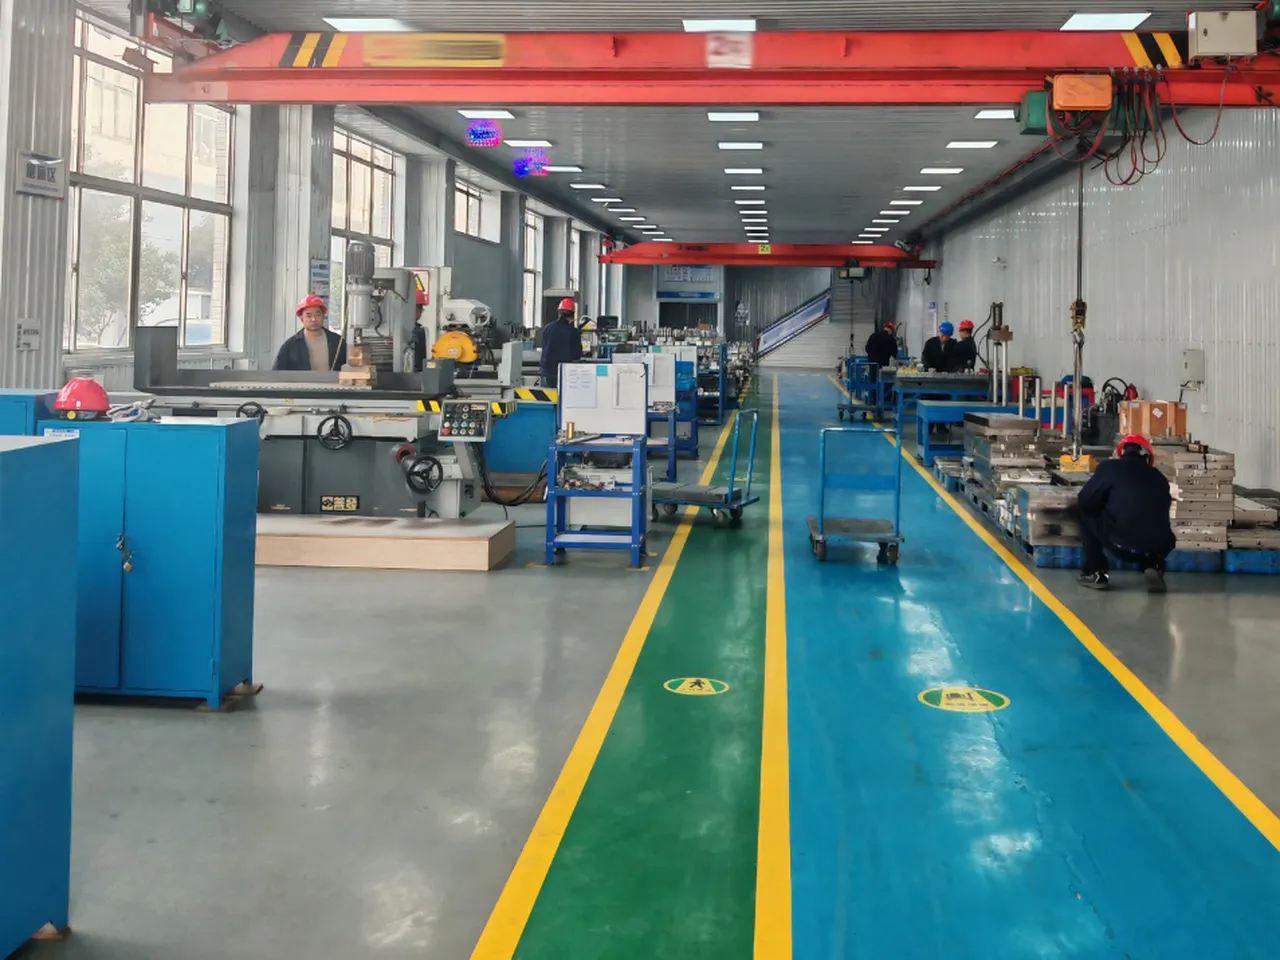
Por que escolher a máquina ISBM da Mexico Ever-Power?
Escolher a Mexico Ever-Power como sua parceira para equipamentos de moldagem por injeção e sopro oferece vantagens distintas, fundamentadas em nossa sólida trajetória e abordagem inovadora. Fundada em 2003, trazemos mais de duas décadas de experiência especializada no desenvolvimento e produção de máquinas ISBM, inspirando-nos em pioneiros do setor e personalizando soluções para priorizar a eficiência operacional e a redução de custos. Nosso portfólio inclui inovações patenteadas em tecnologia de moldagem por sopro, como sistemas servo avançados e designs energeticamente eficientes que reduzem o consumo de energia em até 40%, garantindo que modelos como o Y150-V4 ofereçam confiabilidade excepcional para produção em alto volume sem demandas excessivas de manutenção.
Nossas amplas instalações de 20.000 metros quadrados no México contam com linhas de montagem de última geração e rigorosos protocolos de controle de qualidade, o que nos permite manter padrões consistentes em todos os equipamentos. Somos especializados em máquinas compatíveis com diversos materiais, incluindo PET, PETG, PP, PC e PCTG, atendendo a setores que vão desde cosméticos e bebidas até produtos farmacêuticos e infantis. Essa versatilidade fomentou colaborações com marcas globais de renome, como Estée Lauder, Walmart, Blue Moon e Liby, para as quais fornecemos máquinas personalizadas que aprimoram a integridade do produto e seu apelo no mercado.
O que nos diferencia de outros fornecedores é o nosso foco inabalável no cliente: oferecemos serviços completos e integrados, que abrangem desde projetos personalizados e fornecimento rápido de peças de reposição até consultoria especializada no local, para minimizar o tempo de inatividade. Nossos clientes elogiam constantemente nossa equipe de suporte ágil, composta por profissionais experientes, pela resolução rápida de problemas e pela promoção do sucesso mútuo. Ao priorizar o desempenho estável, a minimização do espaço ocupado e os recursos sustentáveis, construímos uma relação de confiança duradoura e permitimos que as empresas cresçam de forma eficaz em mercados competitivos. Em última análise, a parceria com a Mexico Ever-Power significa aliar-se a inovadores que não apenas fornecem máquinas, mas também impulsionam avanços na moldagem por injeção e sopro em estágio único, ajudando você a alcançar resultados superiores e valor a longo prazo.
 |
 |
 |
 |
Perguntas frequentes
Q: Is the Y150-V4-2 a true drop-in replacement for the Japanese ASB-12M, and can I reuse my existing ASB-12M moulds?
A: Yes. The Y150-V4-2 is fully compatible with Japanese ASB-12M moulds. The machine has been designed with matching platen dimensions, mold stroke specifications, and cooling channel layouts so that your existing ASB-12M tooling can be mounted directly without modification. Ever-Power recommends sharing your mold drawings before shipment so the engineering team can confirm fit and identify any adapter requirements specific to your mold set configuration.
Q: What is the difference between the standard Y150-V4-2 and the full servo YS150-V4-EV variant?
A: The Y150-V4-2 uses three servo pump systems controlling a hydraulic circuit, which delivers high energy efficiency and repeatability for most applications. The YS150-V4-EV full electric injection stretch blow molding machine replaces all hydraulic components with 10 sets of servo motor control systems, eliminating hydraulic oil entirely. This produces a completely oil-free production environment that satisfies GMP pharmaceutical packaging clean-room requirements and eliminates hydraulic oil disposal costs. The EV variant consumes approximately 102.8 KW total versus 53.2 KW for the standard model and is specified primarily for pharmaceutical and food-contact clean-room applications.
Q: What bottle sizes and volumes can the Y150-V4-2 produce?
A: The Y150-V4-2 produces bottles with a body diameter from 26 mm to 118 mm, neck diameters from 15 mm to 83 mm, bottle heights up to 210 mm, and volumes from 20 ml to 2,500 ml. Up to 8 cavities can be produced per cycle depending on bottle diameter. For larger containers up to 20 litres, Ever-Power offers the HGY650-V4 platform, and for bottles requiring more than 8 cavities per cycle or 6 stations, other models in the HGY range are available.
Q: What materials does the Y150-V4-2 process, and does it handle PETG for baby bottles?
A: The Y150-V4-2 is optimised for PET and PETG. PETG is a fully supported material and is the standard choice for baby bottle production on this platform due to its combination of optical clarity, high impact resistance, and sterilisation stability. Ever-Power can advise on the specific screw geometry and barrel temperature profile optimised for your PETG grade. PP processing is also possible with the appropriate screw and barrel configuration; discuss your material specification with Ever-Power engineers during the pre-sale technical consultation.
Q: How much energy does the Y150-V4-2 save compared to a Japanese ASB-12M?
A: The Y150-V4-2 consumes 15% to 25% less energy than equivalent Japanese, European, and American machines. The saving comes from three sources: servo-on-demand hydraulics that use power only when axes are in motion, the nano far-infrared barrel heating ring that transfers heat more efficiently than conventional resistive elements, and the one-step process architecture that eliminates the energy-intensive reheating stage entirely required by two-step machines. Exact savings depend on bottle specification, cycle time, and production hours per day. Ever-Power can provide an energy model for your specific application on request.
Q: Can Ever-Power design and supply custom moulds for a proprietary bottle shape, or only supply the machine?
A: Ever-Power operates as a full-service ISBM mold injection machines supplier, offering both machine supply and complete custom mold design and manufacturing. If you have a proprietary bottle shape, share your 3D CAD data or dimensional drawing with the Ever-Power mold engineering team for a DFM review and quotation. Ever-Power molds are machined to ultra-high precision tolerances and are covered by the same commissioning and support framework as the machines themselves.
Q: What is the typical lead time from order placement to machine delivery?
A: Standard lead time for the Y150-V4-2 is approximately 45 to 60 working days from order confirmation and deposit receipt to factory acceptance testing completion. Ocean freight transit adds 15 to 30 days depending on destination port. If custom moulds are ordered simultaneously, mold lead time is typically 35 to 50 working days and can be aligned with machine production to avoid total project delay. Contact Ever-Power at the time of enquiry to confirm current production schedule availability for your required delivery date.
Q: What after-sales support and warranty does Ever-Power provide for the Y150-V4-2?
A: Ever-Power provides comprehensive after-sales support including on-site installation and commissioning, operator training, and a structured maintenance programme. The standard warranty covers machine defects in materials and workmanship for 12 months from commissioning date. Ever-Power application engineers are available for remote diagnostics via the Inovance PLC communication interface, and a recommended spare parts kit for the first year of operation is provided with each machine. Extended warranty and scheduled maintenance contracts are available on request for customers requiring enhanced service level commitments.
Q: Is the Y150-V4-2 suitable for pharmaceutical GMP production without modification?
A: The standard Y150-V4-2 meets GMP pharmaceutical packaging production standards through its fully contactless 4-station production process. For facilities requiring an oil-free environment, the YS150-V4-EV full servo variant eliminates all hydraulic components. Ever-Power can provide documentation supporting GMP qualification including FAT protocols, IQ/OQ documentation frameworks, and material contact surface declarations on request. The servo-driven bottom-cutting mechanism that replaces the pneumatic system used in Japanese machines is a specific feature that pharmaceutical customers frequently cite as a compliance improvement.
Q: What is the minimum order quantity, and can I order a single machine for evaluation?
A: Ever-Power accepts single-machine orders with no minimum quantity requirement. A single Y150-V4-2 can be ordered for production evaluation, market entry, or as a replacement for a single existing ASB-12M unit. Factory acceptance testing at Ever-Power's facility in Guangdong is available before shipment, allowing you to verify machine performance against agreed specifications using your own material and mold before the machine leaves China. Contact Ever-Power to discuss payment terms, incoterms, and factory visit arrangements for pre-shipment inspection.
Avaliações de clientes
Kim Jae-won, Pharmaceutical Industry, South Korea
"We replaced our Japanese ASB-12M with the Y150-V4-2 about fourteen months ago at our pharmaceutical packaging plant in Incheon. The main reason was GMP compliance because we needed an oil-free option, and the full servo upgrade made that possible. We are running 100 ml oral liquid PET bottles with 6 cavities per cycle now, and the bottle neck dimension rejection rate has dropped below 0.3%, which is much better than anything we were getting before. The Ever-Power engineers spent four full days on-site during commissioning and genuinely made sure our team understood the machine before they left. Very impressed overall."
Priya Mehta, Embalagens de Cosméticos, Índia
"We have been running this ISBM machine for about eight months at our cosmetics factory outside Mumbai and honestly the surface quality improvement over our old two-step machine is night and day. We do luxury glass-look PET bottles for a premium skincare brand and the parting line was always a problem with the previous supplier. With the Y150-V4-2 there is simply no visible seam at all. Our brand customer inspected the first sample batch and approved immediately without any rework request. The energy saving is also real, we measured about 18% reduction in monthly electricity consumption for the same output."
Ricardo Almeida, Food Packaging, Brazil
"Good machine, solid construction. We produce 500 ml cooking oil bottles in high volume at our plant in Sao Paulo and the output rate is noticeably higher than what we were getting from our previous machine. The lead time from order to delivery was about 75 days including ocean freight, which was acceptable. Installation was smooth and the local Ever-Power representative in Brazil was responsive when we had questions in the first few weeks. The one thing I would say is make sure you pre-dry your PET resin properly because we had some quality issues in week two before we sorted out our dryer setup. Once we fixed that everything has been running well."
Hans Bergmann, Personal Care Packaging, Germany
"We purchased the Y150-V4-2 as a direct replacement for ASB-12M equipment and were able to reuse all our existing moulds without modification. This was the key factor in our decision because we had a significant mould investment that we did not want to write off. The machine arrived at our factory in Cologne well packed and with no transit damage. Commissioning took three days and the Ever-Power technician was very knowledgeable. Cycle time is slightly faster than the ASB-12M and bottle quality at least as good, probably better on wall thickness consistency. We would order again."
Nguyen Thi Lan, Baby Products Manufacturing, Vietnam
"The after-sales support from Ever-Power has been genuinely impressive. We had an Inovance servo alarm about four months after installation that we could not diagnose ourselves. I sent a video to the Ever-Power technical team at 10pm and had a response with a diagnosis and parameter correction within 2 hours. Turned out to be a parameter drift in the servo tuning after a power surge. We were back in production the next morning without needing an engineer visit. That kind of remote support capability is really valuable when you are running a production schedule. We produce baby bottle blanks in PETG and the machine handles the material very well."
Ahmed Al-Rashid, Agricultural Chemical Packaging, UAE
"We are a contract manufacturer producing pesticide bottles for several agricultural chemical brands in the Middle East and we needed a machine that could handle a range of bottle volumes from 100 ml to 1000 ml without major changeover downtime. The Y150-V4-2 handles this range well and the mold change procedure is straightforward once your team is trained. The Parker high-pressure valve and the Airtak cylinders are components we can source locally if needed which gives us confidence in the spare parts situation. We have been running 24 hours a day during the peak agricultural season and the machine has held up without unplanned stoppages."
Marco Fontana, Premium Food Packaging, Italy
"I want to highlight the quality of the pre-sale technical support. Before we committed to purchasing we had a lot of questions about whether the machine could produce a specific special-shaped bottle we had designed for a premium olive oil brand. Ever-Power provided detailed feedback on mould feasibility, estimated wall thickness distribution, and recommended screw diameter within a few days and that level of technical depth before a sale gave us real confidence. The machine arrived on schedule and the bottle quality matched the pre-sale analysis very closely. We are very happy and already planning a second unit."
Sofia Ramirez, Personal Care Products, Mexico
"O envio para o México foi muito bem organizado e a Ever-Power forneceu toda a documentação alfandegária, sem erros, o que nos poupou muito tempo na fronteira. A instalação foi concluída em dois dias porque o técnico da Ever-Power foi muito eficiente e claramente conhecia a máquina a fundo. Estamos imprimindo frascos de xampu de 250 ml para um cliente de marca própria e o brilho da superfície e a aderência do rótulo são excelentes. A velocidade de produção é boa e não tivemos problemas significativos de manutenção nos primeiros seis meses. O preço, comparado a máquinas japonesas ou europeias equivalentes, foi um fator importante em nossa decisão e não sentimos que abrimos mão da qualidade."
James Mwangi, Embalagens Farmacêuticas, Quênia
"Operamos uma unidade de embalagens farmacêuticas em Nairóbi e encontrar uma máquina de moldagem por injeção e sopro de estágio único, em conformidade com as Boas Práticas de Fabricação (BPF), com um custo de capital realista para o mercado africano, é realmente difícil. A Y150-V4-2 com a opção totalmente servo nos proporcionou uma máquina que atende aos requisitos de auditoria de nossos clientes da indústria farmacêutica a um preço que realmente podíamos pagar. O CLP Inovance possui uma interface em inglês clara, que nossos operadores aprenderam rapidamente. A Ever-Power também forneceu uma lista detalhada de peças de reposição com as quantidades de estoque recomendadas para o primeiro ano, o que demonstra experiência real no suporte a clientes internacionais. Estamos muito satisfeitos."
Informação adicional
| Editado por | Yjx |
|---|
Produtos relacionados
-
Máquina de moldagem por injeção e sopro em uma etapa Y200-V4-B (4 estações)
-
Máquina de moldagem por sopro e estiramento por injeção em uma etapa Y250-V4-B (4 estações)
-
Máquina de moldagem por injeção e sopro Y200-V3 - Substituta da AOKI SBIII-250LL-50S japonesa
-
Máquina de moldagem por sopro e estiramento por injeção em uma etapa Y50-V3-EV (3 estações)


